Essential Guide to Color Concentrates

What Are Color Concentrates?

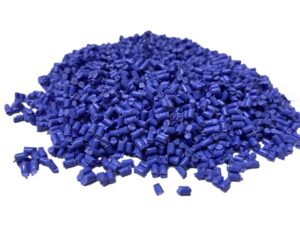
Historically the most common form of Color Concentrates (a.k.a. masterbatches) are colored plastic pellets.  These concentrated colored pellets are typically built to contain 15-50% of specially selected pigments and additives.  The remainder of the recipe is a blend of carrier resin, process aids and binders to support consistency within the virgin base resin.

The initial consideration when designing a plastic component is ensuring the base resin AND the color concentrate are suitable for the selected forming process. Common process examples include injection mold, blow mold, injection stretch blow, compression mold and extrusion.

Each process example will introduce different performance stresses.  For example, during the injection molding process the selected resins, pigments, dyes, and additives must withstand extreme thermal heat, along with increased shear heat generated as the molten material is injected into the mold.

The combined Resin/Color Concentrate blend must also be suitable for its environment. It might need additives to screen out ultra-violet rays, or antioxidants and other stabilizers to protect against polymer degradation, which can lead to discoloration and product failure.

Alternate Path… 100% Pre-Color Compound

Although not largely used, 100% Pre-Color Compound is considered the easiest path to achieve a colored plastic component.  Pre-Color Compound provides the desired end-use color already incorporated within the base resin. This eliminates the need for material blending on the production floor. Pre-Color is often used for very small-size molded components, as the 100% use rate eliminates potential part-to-part color variation.

However, this convenience comes at a very high overall cost and often requires keeping considerable inventory on-hand due to typical industry minimum order requirements. Even with good forecasting, there is a looming threat a program reaches the end of its sales cycle before the pre-color compound inventory is fully depleted.

Color Concentrate Technology Options

The two most widely available choices for Color Concentrates (masterbatches) are either Pellet or Liquid delivery systems.  The question for processors becomes, which is the better option?

Both technologies provide different advantages and challenges.  Below is a brief overview of both liquid and traditional pellet options, followed by the introduction of new pelletized color technology solutions.

Liquid vs Pellet

LIQUID Colorant for manufacturing plastic products:

Plastic Containers

.

Advantages:

  • Effective at extremely low use rates, best suited for tints
  • Less heat history than pellet concentrates
  • Coloring costs can be lower than conventional pellet color 

Challenges:

  • Specialized pumps are required
  • Several pigment and additive limitations
  • Production interruptions caused by container changeover
  • Screw slippage at high use rates, particularly with opaque and pearl
  • Limited application with engineered polymers
  • Not suitable for extrusion blow molding of HDPE bottles
  • Increased housekeeping issues related to spill cleanup and special storage of dedicated hoses
  • Limited shelf life due to product separation, leading to increased costs and wasted color
  • Issues with sustainability due to wasted/residual product and packaging that often requires landfill disposal which is a hidden additional cost
Plastics Technology Article


PELLET Colorant for manufacturing plastic parts and products:

Advantages

  • Pellets are easy to handle and can be dosed accurately through readily available volumetric and gravimetric feeding systems
  • Excellent dispersion
  • Reduced housekeeping and maintenance

Challenges

  • Conventional pellet colorants are typically more costly than liquid colorant due to high let down ratios (LDR)

Ideally, a winning program requires a colorant format that provides all the Advantages… without any of the Challenges.
 

Chroma Color® G Series

Introducing Chroma Color® Corporation’s patented G-Series technologies.

Chroma’s G2®, UltraPETTM and G3® technologies provide vibrant, long-lasting colors essential to meet end-user demands within a convenient Pellet format at the price point in-line with Liquid.

Chroma Color® G-Series

Key Attributes of G2® Color Include:

  • Patented carrier system technology
  • G2® provides substantial Cost-to-Color savings
  • Highest loadings of Organic and Pearlescent Pigments in the industry
  • Highest loadings of UV and AO custom colors in the industry
  • G2® can provide greater than 10% cycle-time reduction
  • Reduced environmental impact, resulting from a decrease in production energy, packaging materials, and CO2 emissions
Chroma Color® Transparent

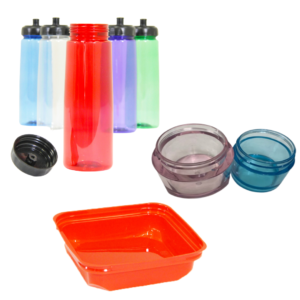
Chroma Color®’s G Series for Packaging Applications

Key attributes of UltraPET®

Color Include:

  • Innovative proprietary carrier system
  • UltraPET® technology allows for component processing at much lower temperature than conventional PET pellet concentrates. Lower process temperatures enable molders to significantly reduce potential heat stress on the pigments and dyes
  • UltraPET® offers exceptionally high loadings of Pigments and Dyes, allowing processors significant economic benefits from low use rates
  • The extremely low use rates (LDR) provided by UltraPET™ can often eliminate the need for drying and recrystallization common in conventional PET pellet concentrates
  • UltraPET® concentrates are available in Mini-Beads for applications sensitive to color dispersion, particularly low-level Tints. Mini-Beads provide higher pellets/gram, increasing pellet distribution, promoting faster incorporation rates, leading to improved color dispersion
  • UltraPET® concentrates are resistant to alcohol and can be formulated in both non-FDA and FDA compliant packages
  • UltraPET® pellet concentrates reduce housekeeping costs compared to the difficulties associated with liquid color
  • NEW – Chroma Color® innovation has developed a unique UltraPET® explicitly designed for use with recycled materials. UltraPET PCR allows brand owners to further increase the levels of PET PCR within their package, supporting increased Sustainability Goals.

 Key attributes of G3® Color Include:

  • Patented manufacturing process technology
  • G3® manufacturing process can be utilized across all major polymers AND carrier systems (standard, G2® or UltraPET™) providing processors the ultimate cost-to-color savings opportunity
  • G3® achieves a further 20% (or more) increased pigment loading levels in polyethylene and polypropylene – without compromising pigment dispersion
  • G3® offers formulations with 40-45% loading of dyes in HIPs, PET, Nylon, Crystal Styrene and Acrylic
  • G3® offers formulations with 50+% pearlescent pigment loadings, nearly doubling the historical industry standard of ~30%

Summary:

As your team reviews various color concentrate options or establishes new performance standards for your plastic products, turn to a trusted colorant supplier to guide you through the process. Chroma Color® Corporation can support your successful product launch, with easy processing, and adherence to all environmental and regulatory requirements… using unique patented technologies that enhance aggressive cost conscience programs. Download the pdf of the article here.

About Chroma Color®:

Chroma Color® Corporation is a technology-leading specialty color and additive masterbatch supplier delivering critical aesthetics, technical innovations, and sustainable solutions to plastics processors and brand owners. Chroma Color®’s growth strategy includes robust organic and inorganic growth and having made six acquisitions over the last three years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant and light management technologies, have delighted customers for over 50 years.
 

Chroma Color® Corporation Acquires Approved Color LLC.

5-9-24, McHenry, IL: Chroma Color® Corporation has acquired Approved Color LLC. a manufacturer of color concentrates and masterbatches in the Northeast.

Founded in 1975, Approved Color has provided quality chromatically matched colorants to the plastics industry. Much of the colorants that Approved Color creates are used in the manufacture of children’s toys, clothing, cookware, food containers, bottles, and other applications.

“In our experience, readiness is paramount in acquisitions. You must always be prepared to seize opportunities as they arise, as you never know when you’ll encounter a company like Approved Color LLC.,” states Joe Herres, CEO, Chroma Color® Corporation. “We are very proud of our acquisition team’s unwavering dedication that has led us to add another high-quality color concentrate and masterbatch manufacturer to enrich our portfolio for our customers.”

Chroma Color® is committed to growing our custom color business through both organic and inorganic activities. The acquisition of Approved Color further bolsters Chroma Color®’s strengths in supporting our customers. The entire team is fully prepared and ready to support Approved Color customers during this time of transition and confident their customers will realize immense benefits from Chroma Color®’s wide range of capabilities.

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, among others. Chroma Color®’s growth strategy includes a deep focus on organic growth as well as inorganic growth through several strategic acquisitions over recent years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its market-leading colorant, has delivered high value to customers for more than 50 years. chromacolors.com.


Chroma Color®® Announces New Chief Executive Officer Joe Herres

®Chroma Color® Joe Herres CEO
Chroma Color® Corporation, leading formulator and supplier of specialty color and additive concentrates and IR absorbing and modifying dyes with an extensive manufacturing footprint throughout the United States, has appointed Joe Herres as Chief Executive Officer effective April 17, 2024 replacing Shruti Singhal. Joe Herres, Chroma’s new CEO commented, “I am very excited to take the leadership role in a business I love and, in an organization, made up of incredibly dedicated and talented team members. Having been the Vice President of Sales and Marketing at Chroma for the past 15 months, I see great opportunities to continue our journey with our customers in helping them grow their business which in turn strengthens Chroma’s ability to partner even more effectively”.


Arsenal Capital Partners Operating Partner and company Chairman George Abd commented, “we are pleased to have Joe take this leadership role bringing with him decades of industry experience and proven success leading and growing businesses. Joe’s deep experience in the plastics industry with a diverse background in polymers and manufacturing processes and his passion for the customer make him uniquely qualified to lead Chroma to the next level. Joe’s strong track record of providing leadership and execution led to exponential growth and market expansion at Spartech, LLC under the ownership of Arsenal and other private equity firms. Joe previously worked for Spartech Corporation both as a public and private business for nearly 20 years and has also worked for Avient (formerly PolyOne). Joe attended Washburn University’s Business Administration and Management program. We want to thank Shruti Singhal for his dedication in leading the organization over the past two and a half years and wish him the best in what we are sure will be a successful next step in his career.”


Chroma Color®®: Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving a diverse range of markets, including packaging, healthcare, pharmaceutical, wire, cable, consumer products, and others. With the acquisition of Epolin, Chroma is also the recognized leader in the near infrared (NIR) absorptive dye industry producing proprietary blends to suit the eye protection and light management sectors. Chroma Color®’s growth strategy includes robust organic and inorganic growth including nine acquisitions. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game changing colorant and light management technologies, have delighted customers for over 50 years. Chroma Color® Corporation is an Arsenal Capital Partners portfolio company. For more information, please contact us: https://chromacolors.com/contact-us/
 

The Manufacturing Institute Honors Chroma Color® Corporation’s, Chief of Human Resources, Cass Birchbauer

Cass Birchbauer, Chief of Human Resources

McHenry, IL, March 8, 2024: The Manufacturing Institute—the workforce development and education affiliate of the National Association of Manufacturers—announced Chroma Color® Corporation, Chief of Human Resource, Cass Birchbauer has been recognized as a 2024 Women MAKE Awards Honoree. This annual national awards program honors women who have demonstrated excellence and leadership in their careers and represent all levels of the manufacturing industry, from the factory floor to the C-suite.

“Receiving this award is incredibly humbling.   Without the dedication to excellence, innovation, and inclusivity of the company I work for—it would not have been possible” stated Cass Birchbauer.  I’m proud to contribute to our company’s success and thankful for the chance to lead impactful initiatives. This award validates why Chroma Color® is really a unique company who never stops pushing boundaries and aiming for greatness.”

The Women MAKE Awards are part of the MI’s Women MAKE America initiative, which is the nation’s marquee program to close the gender gap in manufacturing. Women account for about half of the U.S. labor force but represent less than one-third of the manufacturing workforce. Women MAKE America aims to build the 21st-century manufacturing workforce by empowering and inspiring women in the industry.

“The Women MAKE Awards showcase the vibrant, diverse and rewarding careers in the industry and how women have excelled as manufacturing leaders, paying it forward to inspire and uplift the next generation to pursue opportunities in modern manufacturing,” said Caterpillar Group President of Resource Industries and Women MAKE Awards Chair Denise Johnson.

The Women MAKE Awards gala honors 100 industry leaders (“Honorees”) and 30 rising stars (“Emerging Leaders ”) who have been nominated by their companies as the “go-to” women, recognized for their innovation, dedication, contributions and good counsel. Honorees are further rewarded with access to a two-day leadership development conference in Washington, D.C., in the days leading up to the evening awards gala. Since its launch in 2011, the program has honored and recognized more than 1,400 Honorees and Emerging Leaders.

This accolade serves as a testament to Cass’ unwavering dedication, exceptional leadership, and profound impact on our organization’s human capital strategies within the manufacturing domain. Through her tireless efforts, she has continually elevated our workforce, fostered a culture of innovation and inclusivity, and spearheaded initiatives that have propelled our company forward. Cass also played a pivotal role in creating a culture of ‘ONE TEAM,’ where our focus is on cultivating a safer workplace, encouraging recognition, enhancing communication, providing clear work instructions, promoting feedback, prioritizing training, equipping team members with necessary tools, and advancing an environment of genuine caring, where our team members feel they belong and are set up for success.

“With more than 600,000 open jobs in manufacturing today and the continued need to fill millions more jobs by the end of the decade, it’s critical for manufacturers to engage the largest underrepresented pool of talent: women,” said MI President and Executive Director Carolyn Lee. “The 2024 Women MAKE Awards gala promises to be an inspirational, powerful event, where some of the brightest stars in manufacturing will be recognized for the incredible work they have done—both to grow our industry and to uplift others like them.”

On April 18, the MI will recognize 130 recipients of the Women MAKE Awards in Washington, D.C. The evening will highlight the story of each Honoree and Emerging Leader, including their leadership and accomplishments in manufacturing.

###

ABOUT:

Chroma Color® Corporation is a leading supplier of specialty color and additive concentrates, catering to various industries, including packaging, wire and cable, healthcare, pharmaceuticals, and consumer products, among others. With the acquisition of Epolin, Chroma Color® is now the foremost authority in the near-infrared (NIR) absorptive dye industry, creating exclusive blends tailored to meet the needs of light management applications.

ABOUT THE MANUFACTURING INSTITUTE

The Manufacturing Institute builds, diversifies and strengthens the modern manufacturing workforce, with the goal of furthering individual opportunity, community prosperity and a more competitive manufacturing industry. The MI engages underrepresented communities and shifts perceptions about careers in modern manufacturing, leads skilled training and career development programs, provides thought leadership and research on the changing state of the workforce and builds partnerships to scale up its impact on manufacturing in the United States. As the 501(c)3 nonprofit workforce development and education affiliate of the National Association of Manufacturers, the MI is a trusted adviser to manufacturers, equipping them with solutions for the industry’s toughest challenges. For more information, please visit www.themanufacturinginstitute.org.

Chroma Color®’s Annual Pinnacle Award Winner’s

Chroma Color®'s Pinnacle award

Photo Caption: Chroma Color® Pinnacle Award Winners Celebration held in Nashville, TN: Front Row L-R Gretchen Dragich (SLT), Don Tibbett, Mike Crosby (SLT),Becky Bauer, Mike Johnson, Shruti  Singhal (SLT), Cass Birchbauer (SLT), Kori Bouchard, Kaysi Kaczkowski, Jim Walsh (SLT) Back Row L-R Randy Green, Joe Herres (SLT),LJ Baillargeon (SLT), Glenn Munshaw (SLT), Sandy Ippolito, & David Campbell

*SLT- Senior Leadership team

Chroma Color® announced and celebrated the exceptional achievements of our talented individuals who are our winners of this year’s Chroma Color® Pinnacle Award.  Each year winners are chosen based on their performance and contributions that went “above and beyond” and significantly impacted our company’s growth and success in the prior year. Each winner (and guest) attended a celebration event, award ceremony, and weekend retreat hosted in Nashville, Tennessee.

By working together and going “above and beyond,” Chroma Color®’s 1TEAM will continue to achieve even greater success in the future.

Jennifer Presnell, Quality & Regulatory Affairs, one of the distinguished winners of the Plastics News Sustainability Leaders Award

The leadership team at Chroma Color® Corporation is delighted to announce the recognition of Jennifer Presnell, Quality & Regulatory Affairs, as one of the distinguished winners of the Plastics News Sustainability Leaders in the Plastics Industry award! To qualify for this award, nominees must lead sustainability initiatives at their organization and make a measurable impact on the environment through their efforts. They must also demonstrate leadership through involvement in professional organizations and civic and community initiatives.

Jim Walsh, VP of Technologies at Chroma Color®, remarked, “We are pleased that Plastics News acknowledges the efforts of individuals contributing to the sustainability of plastics companies. Our entire Chroma Color® team has been diligently working towards becoming a reliable sustainable partner for our customers, with Jennifer at the forefront of our initiatives. This year, we witnessed the tangible outcomes of her dedication as we progressed from an EcoVadis Bronze medal to a Silver Medal in 2023, which is why she earned our nomination.”

In emphasizing the importance of responsibility and education, Jennifer stated, “We must be accountable for our actions and strive to educate ourselves, our customers, and the communities we serve for a better collective future. Progress is achieved one step at a time, building on each improvement.” She expressed pride in rallying the company management and employees to establish their sustainability program, which, despite being in its early stages, has already secured an EcoVadis Silver Medal. With ongoing efforts and active projects, the company is committed to reaching its sustainability goals while prioritizing the well-being of its employees and the broader community.

The Chroma Color® team extends heartfelt congratulations to Jennifer, expressing gratitude for her steadfast commitment to steering the company towards a more sustainable future.

Click here learn more about Chroma Color®’s sustainability efforts: https://chromacolors.com/sustainability-2/

#colorconcentrates #plastics #sustainability #plasticsnews #quality #regulatory #ChromaColor

Chroma Color® Corporation Earns APR Design® for Recyclability Recognition for ChromaNIR Technology

 Chroma Color®'s ChromaNIR approved by APR

Chroma Color® Corporation is pleased to announce it has been formally recognized by the Association of Plastic Recyclers (APR) for meeting the highest criteria for recyclability according to the APR Design® Guide for Plastics Recyclability for ChromaNIR.

About APR Design® Recognition:

APR Design® for Recyclability Recognition stands as a third-party endorsement of the compatibility of a package or packaging component with the North American recycling system. This recognition validates that the product has met the most stringent criteria for recyclability outlined in the APR Design® Guide. All components and complete packaging systems are eligible for APR Recognition.

Steve Alexander, the President & CEO of APR, applauded Chroma Color® Corporation’s commitment to enhancing the recyclability of its customers packaging, saying, “APR congratulates Chroma Color® Corporation for taking action to improve the recyclability of packaging and taking the steps to receive APR Design® Recognition. Recyclable packaging means less waste, more efficient use of limited natural resources, and more high-quality post-consumer resin (PCR) for new products.”

James Walsh, VP of Technology at Chroma Color® Corporation, shared his enthusiasm, “Our breakthrough ChromaNIR black technology is a game-changer for PE and HDPE recycling because this formula addresses the challenge of recycling black or dark colors in packaging.”

ChromaNIR’s Innovative Solution: ChromaNIR is a specialized formulation that addresses the crucial need for alternatives to Carbon Black, providing a sustainable solution for recycling black or dark colors in packaging. Chroma Color®’s NIR Sortable Black Technology is built on the foundation of IR reflecting/transparent components, using a unique blend of specialty dyes and organic pigments.

Download our product flyer: https://chromacolors.com/wp-content/uploads/2024/10/Chroma-NIR-APR-Design-Print.pdf

Chroma Color® Corporation invites you to learn more about the environmentally responsible ChromaNIR technology by contacting us at Chroma Color® Corporation Contact Page:

https://chromacolors.com/contact-us/

About APR:

The Association of Plastic Recyclers (APR) is a US-based international non-profit and the only North American organization focused exclusively on improving recycling for plastics. APR’s resources help companies design packaging that can be recycled, support innovations that overcome existing recycling challenges,and encourage stable and reliable markets for post-consumer recycled content. Visit plasticsrecycling.org for more information.

About Chroma Color®:

Chroma Color® Corporation is a leading supplier of specialty color and additive concentrates, catering to various industries, including packaging, wire and cable, healthcare, pharmaceuticals, and consumer products, among others. With the recent acquisition of Epolin, Chroma Color® is now the foremost authority in the near-infrared (NIR) absorptive dye industry, creating exclusive blends tailored to meet the needs of eye protection and light management sectors.

Chroma Color®’s growth strategy includes both organic and inorganic expansion, marked by nine acquisitions in just three years. With over five decades of technical leadership and manufacturing expertise, along with revolutionary colorant solutions, Chroma Color® Corporation continues to delight customers.

Chroma Color® Exhibiting at NPE 2024 South Hall # S25116

Be sure to save the dates May 6- 10, 2024 to meet with the Chroma Color® Corporation & Epolin (Light Management Chemistry) team members to learn more about our plastic color concentrates for consumer,  medical, healthcare, packaging, wire/cable, pipe industrial durables, recreation vehicles,  and more at booth # South Hall S25116 

About Chroma Color® Corporation: 

Chroma Color® Corporation is a leading specialty color concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. With the recent acquisition of Epolin, Chroma is also the recognized leader in the near-infra-red (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors.

Chroma Color® team is dedicated to operating our facilities in a safe and environmentally friendly manner. All of Chroma Color® facilities meet the ISO 9001:2015 standards and the Asheboro facility also meets the ISO/IEC 17025:2017 accreditation. Chroma Color® also earned a Silver Award from EcoVadis in 2023

Chroma Color®’s growth strategy includes robust organic and inorganic growth through nine acquisitions over five years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant, has delighted customers for more than 50 years.

Meet the Chroma Color® team at MD&M West 2024 held Feb 6 – Feb 8, 2024 at Booth # 3995


Informa Markets Engineering West (IME West), home to MD&M West, WestPack, ATX West, D&M West and Plastec West, is the largest annual advanced manufacturing event in the US, bringing together suppliers and buyers for every part of the product development cycle.

Be sure to save the dates February 6-8, 2024 to meet with the Chroma Color® team to learn more about our plastic color concentrates for medical, packaging, additive manufacturing and more at booth #3995

The event is being held in Anaheim, CA at the Anaheim Convention Center.

Not attending the show but want more information? 

Contact Us

#MDMWest, #WestPack, #ATXWest, #DMWest, #PlastecWest

Chroma Color® to Exhibit at Injection Molding & Design Expo Booth – 706

Chroma Color® will be exhibiting at the Injection Molding & Design Expo Booth 706 on September 20-21, 2023 in Novi, Michigan.

Be sure to stop by to learn more about our G-Series Color Concentrates that delivers the Ultimate Solution. . . cleanliness of pellets, reduced cost-to-color, and enablement of sustainability without sacrifice.

Advantages of G-Series

  • Favorable financials with the ease, cleanliness, and convenience of Pelletized Color.
  • Reduced energy consumption through lower processing temperatures and reduced change-over times.
  • Lowest usage rates in the industry yield lower coloring costs and less warehouse space.
  • High loadings and robust formulations overcome the coloring challenges of PCR usage.  These include regeneration of polymer properties, enhanced manufacturing process-ability, end-use performance characteristics, and desired finished goods aesthetics.
  • Formulated to provide optimum color and additive distribution within the final compound and/or molded part.

Chroma Color®’s G-Series provide vibrant, long-lasting colors essential to meeting the demands of compounders, processors, and OEMs.

  • Excellent dispersion and color distribution for optimal aesthetics
  • Reduced carbon footprint (energy, freight, warehouse space, etc.)
  • Matched using our coloring expertise (including special effects)

G-Series are ideal for the following resins

G3 Technology

  • Polyolefins & Polystyrene
  • Elastomeric Resins – TPE, TPO, TPU
  • Engineered Resins – PA, PC, PBT, ABS, ASA, and Alloys,
  • FR Compounds
  • Glass & Mineral Filled Compounds
  • Medical Polymers

 G2 Technology

  • PE, PP, TPE, and TPO with high levels of UV/AO functional additives

ChromaTransparent®

  • PC, PMMA, PET, PETG, Copolyester, MBS (Impact Modified Styrene Acrylic Copolymers), and other clear resins

The show is free to attend. Click here to register online: https://www.ami-events.com/event/0e6056c4-ce50-4b38-a249-393a1d8b3010/regProcessStep1:29e62f9a-6da7-472b-8f1d-88c3b01c33fb?RefId=Website&rp=792924b9-20b3-4864-b600-ad2ef72cc8bd