Once you start exploring the types of industrial textiles made from synthetic plastic resin materials you realize there are many products we use or see daily that fall into this category. Today, even more companies are discovering new capabilities and applications for these materials. Hence, this marketplace continues to grow.
A few reasons for wider acceptance of these materials include flexibility, dry fastness, water absorption and performance in harsh environments. Manufacturers easily gain improved performance with a variety of additives, including colors that ensure the product lasts in a wide variety of environments while also looking attractive.
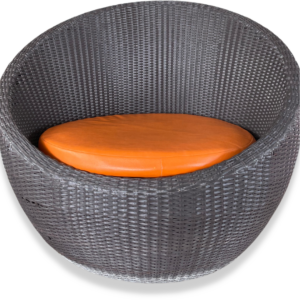
Typical Textile Plastic Resins Capabilities and Applications:
The plastics resins typically used for industrial textiles include: Polyethylene (PE), Polypropylene (PP), Polyvinyl Chloride (PVC), Thermoplastic Polyurethane (TPU) and more.
Polyethylene (PE) is the most common plastic used in the world today. Resistant to tears and rips, the material is extremely rugged and durable, making it suitable for industrial applications. Industrial fabrics made from PE are also lightweight, flexible, and resist soiling and staining. In addition, they are non-absorbent, making them less likely to accumulate dirt/ moisture. They are also resistant to bacteria/ mold.
Polyethylene fabrics are typically chosen for applications such as outdoor chairs, tarps, and tents because they are strong and do not stretch. These fabrics can also be used as gardening mulch to block light contributing to the growth of weeds while letting moisture through. Some other common applications include rope, automotive fabrics and the popular re-usable shopping bag.
Polypropylene (PP) has a higher melting point, making it stronger and lighter than polyethylene. The material is also an excellent insulator and can be engineered into a variety of different products or melted down and recycled into something new. Other important properties of polypropylene include toughness, chemical, water, fire resistance and recyclability.
Textile flooring is the most popular use of polypropylene fiber because it has high abrasion resistance and does not absorb dirt or liquids. Other applications include outdoor carpets, golf and tennis courts, the edges of swimming pools and car interiors. This industrial fabric can also be used in construction–to stabilize the ground or to reinforce roads and banks.
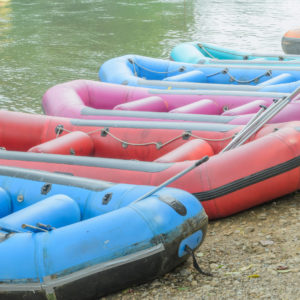
Photo Caption: Marine industrial textiles used for industrial boats
Thermoplastic Polyurethane (TPU) coating:
Thermoplastic polyurethane (TPU) is a very versatile resin. It can be manufactured soft or hard. This material is impact, abrasion, fuel and oil resistant. TPU can be colored and can include additives to protect it from UV rays, funguses and fire.
TPU resin is used to coat textile products such as inflatable boats requiring strength, flexibility, wear resistance, and puncture resistance. It is easy to weld and handle. Other coated textile products include mining screens, conveyor belts, oil booms, barriers/berms, flood spill protection/ control and more.
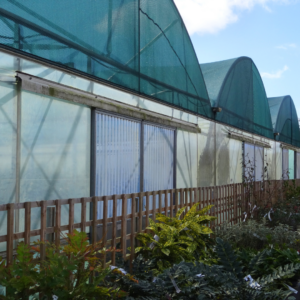
Photo Caption: Industrial textiles are used for greenhouse / nursery protection
Polyvinyl Chloride (PVC) contains halogens like chlorine and fluorine that are widely known for being stable. This chemical stability makes the material resistant to stressors like flame, chemicals and oil.
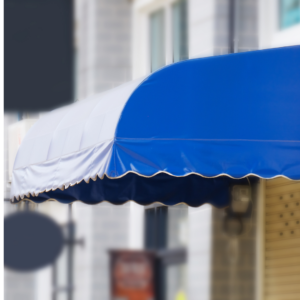
Photo Caption: Business awnings are a popular application for synthetic textiles.
PVC is used for textile applications such as protective suits for firefighters/ military, industrial tarps, conveyor belts, automotive/ RV headliners, marine sails/ lifejackets, awnings, windscreens, athletic mats and much more.
Common Additives for Plastic Textile Fabrics:
Plastic products are often constantly exposed to UV light that degrades the plastic product quickly. But this can be easily prevented with the addition of a UV additive. Other additive options include flame retardants, anti-static, processing stabilizers, antimicrobial agents, and more. If you think you need additional additives work with your supplier to help you decide what you need and how they will perform for each resin base.
Color Concentrates for Plastic Textiles:
One of the biggest challenges in color use for plastic textiles is matching them to the resin that is used. Initiate a conversation with your color supplier about the resins’ viscosity and melt processing temperatures. This will make the decision on carrier resin, pigments, stabilizers and other additives necessary for the application much easier.
Then, depending upon the material and application, the carrier resin used in the concentrate will be about 30-50%. It is also important to review the molecular weight of that carrier or melt flow rate (MFR). The color concentrate should have higher MFR than the base resin that is being colored in order to produce a good colored part.
After the resin has been clearly established, your conversation can move to color selection. Typically, your supplier will have sample chips or Pantone color charts to pinpoint the desired color for each plastic product or part.
During this selection, bear in mind that colors can look different on the material depending on its gloss, filler and look. For example, lighter colors such as red, orange, and yellow could change color faster compared to darker colors like blue or green.
Looking for unique or custom colors to separate you from your competitors or one that needs to stand out for safety applications such as life jackets or inflatable boats? You can count on color supplier’s like Chroma Color® Corporation to help you choose the best options for your application.
About Chroma Color® Corporation:
CHROMA COLOR Corporation’s textile team has experience helping customers looking for color industrial textiles made from PVC, PP, TPU and PE materials.
Our capabilities include:
- Fully equipped laboratories to formulate thermoplastics colors and compounds. Colorists thoroughly trained in the theory and practice of spectrophotometry, color measurement, and color science
- Color formulation, color control, color tolerances, standards, and color faults and their evaluation
- All facilities meet ISO 9001:2015 standards
- Adherence to the following regulatory guidelines: FDA Food Contact Compliance, HMF Heavy Metal, Free Formulation, EU & other Global Standards
- Availability to provide color concentrates in dice, strand, underwater cut, and/or pulverized pellet geometry
Chroma Color® Corporation is a leading specialty color and additive concentrate supplier of the highest quality and the shortest lead times in the plastics marketplace. The business exceeds $160 million in sales due to solid organic growth and targeted acquisitions. Chroma’s extensive technical and manufacturing expertise coupled with its game-changing colorant technologies have surprised and delighted customers for over 50 years in markets such as: packaging, wire and cable, building & construction, consumer, medical, healthcare, lawn & garden, durables, sanitation, recreation and leisure, transportation and more.
Download this material as a PDF