Plastic Packing Trends and How to Choose the Best Color Concentrates to Meet These Trends
Trends in Packaging in 2026 and Beyond

A major trend in packaging is the shift toward smarter, advanced solutions. These include digital watermarks for better sorting and recycling, as well as sensors that track freshness and supply‑chain conditions. Brands are also reducing material use through lightweight designs and adapting packaging for e‑commerce and convenience. Overall, plastic packaging is evolving to balance cost, functionality, and sustainability amid expanding consumer and regulatory pressures.

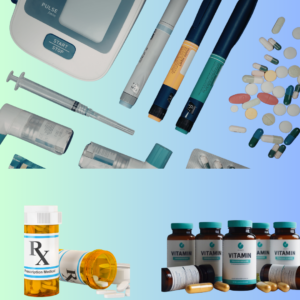
The rapid adoption of GLP‑1 drugs is significantly affecting demand for plastic packaging. These medications rely on plastic‑heavy delivery systems—such as single‑use autoinjector pens, protective caps, and sterile packs—driving large‑scale production and investment in medical‑grade plastics. They also require cold‑chain packaging due to refrigeration needs.

Chroma Color for Medical products and devices

Because GLP‑1 drugs reduce appetite, consumers are buying less food, especially packaged snacks, lowering demand for some plastic food packaging. This decrease is partly offset by growing interest in smaller portions and resealable formats. At the same time, the rise in single‑use medical plastics, including injector pens and sharps containers, is increasing waste concerns and highlighting the need for more eco-friendly materials and recycling solutions in healthcare.

How to Choose the Right Color Concentrate to Meet Your Current Plastic Packaging Needs

It is essential in today’s business environment to choose the best color concentrate technology that delivers highly consistent, high-performance color to your packaging, improving both processing effectiveness and final product quality. Look for advanced formulations that allow for lower let-down ratios, meaning manufacturers can achieve the same color intensity with less material—cutting overall costs and improving sustainability. The technology ought to enhance dispersion, resulting in smoother color uniformity, fewer production defects, and more predictable performance across multiple resin types and applications.

Chroma Color Concentrates Pellets

You should also ask yourself: Is this color concentrate engineered for faster processing and reduced cycle times to ensure throughput without impairing color precision or durability? Does the concentrate’s thermal stability support demanding packaging processes, including thin-wall designs and high-speed extrusion or injection molding? Together, these advantages will help you boost packaging performance, reduce waste, and improve operations.

The Benefits of Switching from Liquid Color to Color Concentrates:

Switching from liquid color to high-performance color concentrate technology offers several important advantages that can significantly improve manufacturing performance and reduce total production costs. High-performance systems provide far more precise colorant delivery, resulting in consistent, repeatable color with minimal variation from batch to batch. Because these technologies meter color directly into the process, they eliminate the mess, storage challenges, and contamination hazards often associated with liquid color. They also reduce cleanup time and simplify changeovers, permitting operators to move between colors more quickly with less downtime. In many cases, you can achieve the same—or better—color strength while using less additive. The combination of accuracy, cleanliness, reduced waste, and lower operating costs makes these systems a strong upgrade over traditional liquid color.

How Color Concentrate Drug Master Files (DMFs) for Medical Plastic Packaging Makes Your Life Easier

Drug Master Files offer medical packaging companies a substantial regulatory and operational advantage by providing pre-vetted, FDA-reviewed documentation for colorants used in pharmaceutical and healthcare products. This reduces the burden of material qualification, speeds time to market, and simplifies compliance for devices such as syringes, caps, connectors, and diagnostic components. With DMFs in place, you can be confident that your color concentrate is safe, consistent, and traceable—critical factors for your medical-grade packaging that must meet strict performance and regulatory requirements.

A Good Color Concentrate Option for Your Plastic Packaging
Chroma Color G3 Logo

Chroma Color’s G3 technology delivers strong value by providing high-efficiency color concentrates that improve processing performance while cutting overall material costs. G3’s advanced dispersion enables rich, uniform color at significantly lower let-down ratios, helping manufacturers use less concentrate without sacrificing quality. Chroma’s patented G3 technology can also provide highly loaded concentrates containing laser-marking additives. The formulation also allows faster cycle times, excellent thermal stability, and cleaner processing, which together reduce waste, improve production efficiency, and improve sustainability across a wide range of plastic packaging applications.

To learn more about G3 and Chroma Color Corporation, visit: chromacolors.com.
Chroma Color® Expands Footprint with West Coast acquisition of Spectra Color

Chroma Color® and Spectra Color logos

<12/20/2024>, McHenry, IL: Chroma Color® Corporation (“Chroma Color®” or “Chroma”) continues to grow its manufacturing footprint along with its portfolio of colorant and additive technologies with its recent acquisition of Spectra Color, Inc. (“Spectra Color” or “Spectra”) a custom manufacturer of colorants and pre-colored resin compounds. Spectra also manufactures a proprietary resin primarily made from linear low-density polyethylene, predominantly used in the rotational molding industry.

Located in Corona, California, Spectra is a leading provider of masterbatch and color-matching services with custom blending capabilities. Founded in 1976, they have supplied the plastic industry with high quality thermoplastic compounds, colorants, additives, and value-added resins for over 45 years. Spectra serves diverse end-markets, including medical, healthcare, agriculture, consumer products, among others.

Spectra CEO, Bob Shedd, said, “We are thrilled to join forces with Chroma Color®. Chroma’s strong market reputation and shared vision for the business make this partnership a perfect fit. By combining  our technological expertise, we can deliver a powerful competitive advantage, enhance performance, and create even greater value for our customers.”

“Chroma Color® is dedicated to driving growth through both organic initiatives and inorganic growth opportunities. The acquisition of Spectra Color underscores our commitment to expanding our geographic reach and enhancing our product offerings to better serve our customers,” stated Joe Herres, Chroma Color® Corporation, CEO. “The entire team is fully prepared to support Spectra’s customers during this transition, and we are confident they will experience significant value from Chroma’s extensive capabilities and resources.”

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, among others. Chroma Color®’s growth strategy includes a deep focus on organic growth as well as inorganic growth through several strategic acquisitions over recent years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its market-leading colorant, has delivered high value to customers for more than 50 years. chromacolors.com

Chroma Color® Exhibiting at Compounding World 2024 Booth # C1526

Chroma Color® Compounding World 2024

Chroma Color® Corporation is a leading specialty color concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. With the acquisition of Epolin, Chroma is also the recognized leader in the near-infrared (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors. Stop by booth C1526 to talk to the Chroma Color® about our color concentrates and masterbatches that includes G-Series, UltraPET, ChromaPCRPET, ChromaNIR, Bio-Compostable option, and more.

The Compounding World Expo is being held in Cleveland, OH, on November 13-14, 2024. Cleveland is the plastics hub of North America and this event caters to the entire compounding supply chain where you can network with peers, gain insights from experts, and explore cutting-edge exhibits – all for FREE. To register visit: https://na.compoundingworldexpo.com

Also you can gain a broader perspective with the co-located expos: Plastics Extrusion World Expo, Plastics Recycling World Expo, and Polymer Testing World Expo that offer cross-industry insights. Our dynamic conference program features technical presentations, industry debates, and insightful seminars across four dedicated theaters.

Chroma Color® Exhibiting at NPE 2024 South Hall # S25116

Be sure to save the dates May 6- 10, 2024 to meet with the Chroma Color® Corporation & Epolin (Light Management Chemistry) team members to learn more about our plastic color concentrates for consumer,  medical, healthcare, packaging, wire/cable, pipe industrial durables, recreation vehicles,  and more at booth # South Hall S25116 

About Chroma Color® Corporation: 

Chroma Color® Corporation is a leading specialty color concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. With the recent acquisition of Epolin, Chroma is also the recognized leader in the near-infra-red (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors.

Chroma Color® team is dedicated to operating our facilities in a safe and environmentally friendly manner. All of Chroma Color® facilities meet the ISO 9001:2015 standards and the Asheboro facility also meets the ISO/IEC 17025:2017 accreditation. Chroma Color® also earned a Silver Award from EcoVadis in 2023

Chroma Color®’s growth strategy includes robust organic and inorganic growth through nine acquisitions over five years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant, has delighted customers for more than 50 years.

Chroma Color®’s patented G-Series Technologies deliver the Ultimate Solution for Compounders

Chroma G Series Logo

Chroma Color®’s patented G-Series Technologies deliver the Ultimate Solution for Compounders . . . cleanliness of pellets, reduced cost-to-color, and enablement of sustainability without sacrifice.

Advantages of G-Series Masterbatches

  • Favorable financials with the ease, cleanliness, and convenience of Pelletized Color.
  • Reduced energy consumption through lower processing temperatures and reduced change-over times.
  • Lowest usage rates in the industry yield lower coloring costs and less warehouse space.
  • High loadings and robust formulations overcome the coloring challenges of PCR usage.  These include regeneration of polymer properties, enhanced manufacturing process-ability, end-use performance characteristics, and desired finished goods aesthetics.
  • Formulated to provide optimum color and additive distribution within the final compound and/or molded part.

Chroma Color®’s G-Series masterbatches provide vibrant, long-lasting colors essential to meeting the demands of compounders, processors, and OEMs.

  • Excellent dispersion and color distribution for optimal aesthetics
  • Reduced carbon footprint (energy, freight, warehouse space, etc.)
  • Matched using our coloring expertise (including special effects)

G-Series Masterbatches are ideal for the following resins

G3 Technology

  • Polyolefins & Polystyrene
  • Elastomeric Resins – TPE, TPO, TPU
  • Engineered Resins – PA, PC, PBT, ABS, ASA, and Alloys,
  • FR Compounds
  • Glass & Mineral Filled Compounds
  • Medical Polymers

 G2 Technology

  • PE, PP, TPE, and TPO with high levels of UV/AO functional additives

ChromaTransparent

  • PC, PMMA, PET, PETG, Copolyester, MBS (Impact Modified Styrene Acrylic Copolymers), and other clear resins

Download the Full PDF