Overview of Coloring Plastic Pipe

The pipe market is very competitive. Pipe manufacturers are continually looking for ways to reduce cost while delivering products that meet performance expectations set by customers, codes and standards (ASTM, NSF, NEMA, etc.). Chroma Color® Corporation develops pigments/colors through internal and industry partners related to research, education, technical expertise and trade associations like the Plastic Pipe Institute (PPI) https://plasticpipe.org/index.html allows Chroma Color® to deliver superior and environmental (SUSTAINABILITY HMF) product to the pipe industry.

There are five major markets for a plastic pipe; each has its own unique needs and regulations. These five markets include:

-Building & Construction

-Drainage Pipe

-Energy Piping Systems

-Municipal & Industrial

-Power & Communications


Plastic pipe and conduit color-coded by their end-use application, such as:

-Blue = Potable Water

-White = Irrigation and Water

-Green = Sewer

-Purple (Lavender) = Reclaimed Water

-Gray = Electrical Conduit

-Orange = Telecommunication, conduit

-Yellow = Natural Gas (methane or propane) oil

-Red = Electric Power Lines, Lighting Cable

 Plastic Pipe Resins:

One of the biggest challenges related to coloring a plastic pipe product is accurately matching the desired color in the specific resin. It is critical to establish a partnership with your color & additives supplier early in the development process to meet specific color and the performance attributes.

The colorant supplier must consider the unique resin, color, and performance requirements as they formulate for the application. Each resin is unique (viscosity, melt processing temperatures, natural resin color, and more). Your color supplier can assist with critical application decisions from the onset regarding the carrier resin, pigment systems, stabilizers, and other additives.

The resins primarily used for pipe include:

HDPE: High-Density Polyethylene

MDPE: Medium Density Polyethylene

PEX: Crosslinked Polyethylene

PE-RT: Polyethylene of Raised Temperature

PP-R and PP-RCT: Random Copolymerized Polypropylene

PEX-AL-PEX: Multilayer or Composite PEX Tubing

In general, the features and benefits of the high-performance high-temperature plastic-piping systems include:

  • Ease of installation (Coil Pipe)
  • Corrosion resistance
  • Safety of potable Water
  • Reliable fitting and joining options
  • Lightweight, ease of transportation and handling
  • Proof of long-term reliability with over decades of use around the world (100 year life expectation) with proper manufacturing and installation.

Types of Pipe and Resins

Municipal and Industrial Water Applications

For municipal and industrial applications, high-density polyethylene (HDPE) pipe is recommended. HDPE’s heat-fused joints create a leak-free pipe structure. HDPE pipe is chemical, abrasion, fatigue, seismic, and corrosion-resistant.

Conduit

High-density polyethylene (HDPE) resin is also used for the conduit to protect electrical power and telecommunications cables. It is available in long coil lengths to reduce joints and installation time. HDPE conduit is also available in a variety of sizes, colors, dimensions, and lengths. Typical applications include:

–Telecommunications

-CATV

-Highway lighting

-Underground utilities.

–Premise (Riser and Plenum) conduit has specific characteristics and flame retardant ratings for use as nonmetallic raceways in buildings.

Color Selection:

After establishing the resin, your conversation moves to color selection. Typically, your supplier has color sample chips or Pantone color charts to pinpoint the desired color for each plastic product or part.

During this selection process, colors may differ depending on gloss, grain, filler, resin type, light sources, and other factors. Knowing this in advance allows the color supplier to choose high-performance pigments that are more light stable than typical workhorse pigments.

There is also much pressure to eliminate the use of heavy metals (HM) pigments in favor of more environmentally friendly options. You need to ask your color concentrate supplier if the pellets include Heavy Metal Free (HMF)* or Heavy Metal (HM) pigments.

*Chroma Color® Corporation meets ASTM F2160 − 22 requirements that requires the use of HMF pigments and eliminates the selection of HM.

In addition, heavy metal-based heat stabilizers have traditionally been used with HDPE and/or polyethylene pipe. These include Lead and Cadmium Salts. Such environmentally unfriendly chemicals are rapidly being replaced with non-heavy metal stabilizers, such as calcium stearate.

A pipe that uses HMF (Heavy-Metal Free) stabilizers provides the end-user with the confidence of zero toxicity from heavy metals.. These include Lead and Cadmium Salts. Such environmentally unfriendly chemicals are rapidly being replaced with non-heavy metal stabilizers, such as calcium stearate. A pipe that uses HMF (Heavy-Metal Free) stabilizers provides the end-user with the confidence of zero toxicity from heavy metals.

Pipe exposed to Ultra Violet Light needs protection from the damage caused over time. Chroma Color®’s patented G series can have a stabilizer with UV resistant material to provide some protection from UV damage.

Chroma Color®’s patent G2 and G3 also provides a cost-effective solution for solid wall pipe and vibrant co-extrusion skin colors.
ChromaGSeries

BASICS of ChromaGSeries PATENTED G2, G3 COLOR TECHNOLOGY

Highly loaded concentrates have become a cost-effective alternative to standard color products because they require less concentrate to achieve the same results and blend with resin more efficiently.

The patented G2 formulation ingredients enable Chroma Color® to boost loadings of pigments and additives up to twice what was considered feasible in traditional color and additive concentrates.

– Typically, a G2 formulation contains up to about 80% active ingredients, some as high as 85%. For some pipe applications, we can load up to 60% additives.

– A high concentration of color and additives is just one aspect of G2 technology. The technology also allows us to dial in melt flow to enable the processor to produce uniformly colored parts with color use rates as low as half a percent.

Patented G3 reduces cost and eliminates processing headaches. It achieves even more significant improvements through a total system approach. Key attributes and advantages include:

– Used with any resin system except PVC

– It delivers 20% or more increased pigment loading than G2 in Polyethylene & Polypropylene without compromising pigment dispersion and distribution

– G3 offers formulations with 40% of dyes in HIPS, PET, Nylon, Crystal Styrene, and Acrylic.

– It offers formulations with 50% or more pearlescent pigment, nearly doubling the former industry standard of 30%

-Heavy Metal Free

CHROMARK® is Chroma Color®’s laser marking additives to help control marking behavior over a broad class of resins and pigment chemistries. The Chroma Color® team can help you select the right colorant and additive package to ensure you obtain the ideal laser mark for your product at an economical cost-to-color.

With our in-house NIR Laser, we help you optimize the marking behavior and laser settings for various resins, including ABS, PE, PP, LDPE, HDPE, Co-Polyester, PBT, Polysulfone, GPPS, HDPE, Nylon, Acrylic, PVC, Polyacetal, and Polycarbonate. Besides, Chroma’s patented G3 technology can also provide highly loaded concentrates with a laser-marking additive.

Chroma Color® Plastic Pipe Case Studies

Wire and Cable Application:

A manufacturer of electrical wire was looking for a better color concentrate option for their product line. Our wire and cable research team developed a highly loaded PVC concentrate that is producing the following results:

1- Reduction in Let Down Ratio (LDR) with an LDR of 0.5% reduced inventories and upfront cost

  1. The low LDR reduces the number of spark outs (if any) that reduces machine downtime and increases utilization
  2. Black 508/2006 PVC unique formula reduced shear heat to allow increased line speeds on thin gauge products
  3. The unique formula enhances the black appearance on a retail shelf by giving your coiled wire a shine instead of a typical stock black dull appearance.
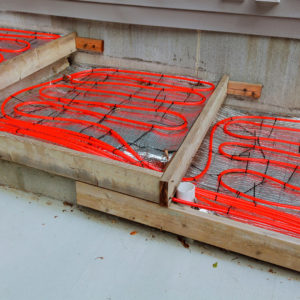


Radiant Pipe Application:

– G2 used for a high-temperature pipe used for a radiant application.

– Co-Extruded outside skin polyethylene raised temperature PERT-PE skin colors to reduce the overall cost of pipe. 3,000-4,000 of an inch thick skin

– Lower Letdown Ratios of .75% Achieved

– Red, Blue and White Colors Available

– UV additives used to prevent fading

– Other applications for this technology include high-temperature for building construction, hot and cold water pipes, and business.

Click Here To Download The Full Article As A PDF 

Advances in Color For Medical Plastics for Today and Tomorrow

With an increasing demand in the medical plastics market globally, manufacturers are pioneering high-quality resins that raise the standards of excellence in health care. Advancements in plastics are curbing medical costs and enhancing patient safety.

Medical-grade plastics are designed to meet stringent regulatory requirements and may also be chemical-, corrosion- and temperature-resistant. Unlike the glass, ceramic and metal products of yesteryear, plastics create low-cost, lightweight and durable equipment and devices that are easier to use and more comfortable for patients. With the over-65 population in the United States expected to outnumber the under-18 age group by 2034, there’s never been a bigger need for advances in medical plastics.

With the increased demand, the medical plastics industry has been utilizing advancements that are improving product performance and design, including:

  • End-to-end traceability

Since 2013, the U.S. Food and Drug Administration (FDA) has required numeric or alphanumeric codes on specific medical devices to improve traceability. These unique device identifiers (UDI) help manufacturers track medical device adverse events and identify the need for recalls.

Beginning on Sept. 24, 2020, all Class I devices and unclassified devices must bear a UDI label or mark. Class I includes bandages and nonelectric wheelchairs and accounts for 47% of medical devices.

End-to-end traceability provides information about the lifecycle of the product, from its origins to usage. It also helps drive down counterfeiting, minimizes liability and provides healthcare workers and patients with peace of mind.

  • ISO certification

Medical plastics manufacturers seek International Organization for Standardization (ISO) certification because it demonstrates excellence and a commitment to global standards. The ISO – an independent, non-governmental organization – establishes guidelines, specifications and requirements to ensure safety and quality in industries that include medical plastics. Two ISO standards have become synonymous with excellence in medical plastics:

  • ISO 9001

As the ISO’s flagship quality management standard, the ISO 9001 certification confirms a company’s abilities to provide consistent quality, meet customer needs and comply with regulatory requirements. The latest revision, ISO 9001:2015, is based on the plan-do-check-act (PDCA) cycle, a four-step model for continuous improvement. After a company has integrated ISO 9001 standards, a third party to verify compliance regularly audits it.

  • ISO/IEC 17025

Used in a laboratory setting, ISO/IEC 17025 stipulates the technical competencies and management system requirements to deliver valid test results and calibrations consistently. Due to the universally accepted set of standards, ISO/IEC 17025 allows for collaboration among laboratories worldwide.

  • Quality materials

Today, manufacturers are less concerned with the price of materials than the quality to align with the needs of the market and changes in government regulations.

High-caliber medical thermoplastics – such as polyvinyl chloride (PVC), polyethylene (PE) and polystyrene (PS) – and thermoplastic elastomer (TPE) compounds made with FDA-compliant ingredients remain critical to the medical device design process. At the same time, the market for polycarbonates, ABS, polyamides and polyetheretherketones (PEEKs) is expanding.

  • Dynamic color and antimicrobial properties

Healthcare providers are continually seeking new approaches to influence patients. Color and antimicrobial properties, in different ways, help achieve results.

Color helps users recognize tools, remember instructions and identify instruments. In medical plastics, vibrant and long-lasting colors are essential to patient and user safety. Companies that include Chroma Color® Corporation have been developing technology that makes the colorant less expensive without sacrificing quality. Chroma Color®’s G2® and G3® pelletized colorant technology allow for superior color uniformity when compared to conventional pellets or liquid colorant and low let-down ratios, which also reduces production costs.

Antimicrobial additives inhibit mold, fungi, mildew and bacterial growth and when blended with plastic resins also help fight stains and odor. Chroma Color® offers two types of antimicrobial additives: MicroBlok®S and MicroBlok®Z.

In addition, medical plastics manufacturers are exploring 3D printing and are increasingly utilizing extruders to create tubing, films and sheets. The Plastics Industry Association said plastics are vital for safe patient care today and in the future.

“Plastics are at the forefront of innovation in a wide range of medical specialties,” the association said in its Plastics Market Watch report. “But even before scientists and material engineers develop healthcare applications, the plastics value chain is making innovations in manufacturing and supplying plastics—from the simple to the complex that transform how patients are treated and live their lives.”

About Chroma Color® Corporation

Chroma Color® Corporation is a technology-leading specialty color and additive concentrate supplier in the plastics marketplace. Chroma’s extensive technical leadership and manufacturing expertise coupled with its game-changing colorant technologies have surprised and delighted customers for over 50 years. Chroma’s wide-ranging markets include packaging, wire and cable, building and construction, consumer products, medical, healthcare, lawn and garden, durables, sanitation, recreation and leisure, transportation and more.

Plastic Colorant Options 101: Pellet vs Liquid

Color is a critical feature in consumer packaging that enables brands to create differentiation and recognizable identity on shelf. Major brands and their packaging supply partners are rethinking their colorant strategy.

How do you find the right value-added color supplier? Most color suppliers have a fixed portfolio of either liquid colorants or traditional pellet colorants, thereby leaving processors confused about choosing the best colorant technology to accomplish their goals.

Both technologies have advantages and disadvantages. Below, is a quick overview of both liquid and traditional pellet options followed by two case studies in which color-processing challenges were overcome using a new pelletized color technology solution.

Liquid vs. Pellet:


Liquid Colorant for manufacturing plastic products:

Advantages:

  • Effective at extremely low use rates.
  • Good for tints
  • Good Color distribution
  • One less heat history than pellet concentrates
  • Coloring costs may be lower than conventional pellet color

Challenges:

  • Specialized pumps are required
  • Several pigment and additive limitations.
  • Screw slippage may occur at high use rates
  • Limited application with engineered polymers
  • Not suitable for extrusion blow molding of HDPE bottles
  • Production interruptions caused by container changeover.
  • Increased housekeeping issues related to spill cleanup and storage of dedicated hoses.
  • Limited shelf life due to product separation that ends up increasing costs and wasted color.
  • Issues with sustainability due to wasted/residual product and packaging which often requires landfill disposal.

Pellet Colorant for manufacturing plastic parts and products:

Advantages

  • Pellets are easy to handle
  • Application through readily available volumetric and gravimetric feeding systems
  • Excellent dispersion
  • Reduced housekeeping and maintenance

Challenges

  • Conventional pelletized colorants are more costly than liquid colorant due to high let down ratios.

Ideally, a winning program requires a colorant format that provides ALL the Benefits and without ALL the Challenges…

Attached are two case studies illustrating how the patented Chroma Color® G-series pelletized colorant technology resolved challenges faced by major brand owners and their plastics processors with conventional pelletized colorants and liquid colorants.

CASE STUDY #1

Mock up empty container bottles for cosmetic cream, isolated on white background with clipping path.

Overcoming Processing Limitations of Pearlescent Liquid Colorant

Liquid color can be very complex and typically requires extra care during processing to ensure that specified color appearance is achieved.

A case in point is the use of pearlescent liquid colorants for a large commercial brand’s package. Although the liquid colorant initially met the basic aesthetics and manufacturing needs, continual processing challenges persisted with high scrap rates and inconsistencies.

Specifically, it was determined ingredient separation within the liquid masterbatch was the root cause of the visual inconsistencies. Additionally, the ingredient separation required liquid colorant agitation that frequently interrupted production scheduling. Overall production costs became substantially higher than anticipated (quoted) and production throughput was negatively impacted.

Even with the recent advancements in material handling and liquid feeding systems, liquid colorants remain messy to handle, which adds to both processing labor costs and changes to housekeeping practices. Due to these persistent obstacles, the packaging development team decided to seek an alternative product to achieve the desired pearl color.

The Solution: Chroma Color®’s patented G3 pellet technology

The packaging team immediately benefited from the switch because:

  • G3 does not have any shelf life limitations
  • G3 reduced flow lines that frequently appeared on components produced using pearlescent liquid colorants
  • G3 enabled substantially faster and more cost-effective color changeovers with less purge and reduced downtime
  • G3 inventory was fully consumed, with no residual waste.

Chroma Color®’s patented G3 colorant was ultimately selected to replace all the liquid colorants within the final package. Gravimetric pellet color feeders were integrated on the production line, resulting in significant overall cost reductions.

For more information about patented G2 and G3 pellet technology from

Chroma Color® Corporation, visit:

https://chromacolors.com/g2-and-g3/

CASE STUDY #2

Eliminating Instability of Teal Colorant and Inefficient Let-Down Rates

Blank dispenser and bottles of cosmetic products with turquoise lids

The particular Teal color-space is critical for this brand’s identification, yet it faced multiple color related concerns such as inconsistencies amongst the individual components.

The part-to-part inconsistency forced the Processor to consume the current colorant at substantially higher use rates to achieve visual color uniformity. These higher use rates forced production inefficiencies, larger than desired colorant inventories and elevated levels of finished component inventory to ensure required lead times were maintained.

Consequently, the Brand Packaging team and Processor jointly began searching for an alternative colorant to resolve the multiple challenges of color stability, processing difficulties, excessive use rates and overall package cost. During their investigations, we introduced Chroma Color®’s patented G-series colorant technologies. The G-series technology includes both G2 (recipe system) and G3 (manufacturing technology). Molding trials on both technologies were initiated, to identify the most appropriate and beneficial package.

The Solution: Chroma Color®’s patented G2/G3 technology

  • G2/G3 system combination provided superior color dispersion eliminating color variation
  • G2/G3 combination reduced the use rate from 4% to 1.5% LDR, lowering the overall cost-to-color expense
  • G2/G3 system combination provided faster cycle times, more cost-effective color changeovers with less purge and reduced downtime.

Chroma Color®’s patented G2/G3 colorant package was selected to achieve the desired Teal. The lower letdown ratios, along with the processing benefits of the G-series allowed the molder to meet required their production demands. Further, with the lower color requirements, coupled with the gained production efficiencies, provided desperately needed warehouse storage space.

The numerous benefits brought to the program via Chroma Color®’s patented G2/G3 combined technologies eventually led to a complete switch on ALL colorants for this Brand’s needs.

For more information about patented G2 and G3 pellet technology from

Chroma Color® Corporation, visit:

https://chromacolors.com/g2-and-g3/

To download this article: Liquid vs Pellet

Chroma Color® Corporation is a technology-leading supplier of specialty colorants and additive concentrates. Chroma’s extensive technical and manufacturing expertise coupled with its game-changing colorant technologies have surprised and delighted customers for over 50 years in markets such as: packaging, consumer products, wire and cable, building & construction, medical & healthcare, lawn & garden, durable goods, sanitation, recreation & leisure, transportation and more.

References:

1-https://books.google.com/books?id=urctkFROYbkC&pg=PA439&lpg=PA439&dq=liquid+color+vs+pellet&source=bl&ots=luqZQ-mkoB&sig=-uRUrvG7pSfcmfFA12qs4YlfXZQ&hl=en&sa=X&ei=S2Y1VZHHCrGOsQSOl4D4Ag&ved=0CDYQ6AEwBw#v=onepage&q=liquid%20color%20vs%20pellet&f=false

2- https://books.google.com/books?id=9IZSW9BVCyAC&pg=PA297&lpg=PA297&dq=liquid+color+vs+pellet&source=bl&ots=Q63Bdp6GLe&sig=FZA4FTDryATy0QapU6v9sLQzU1o&hl=en&sa=X&ei=S2Y1VZHHCrGOsQSOl4D4Ag&ved=0CDQQ6AEwBg#v=onepage&q=liquid%20color%20vs%20pellet&f=false

Advantages of a Color Masterbatch for Molding Plastics

Typically, a masterbatch is available in either a liquid or pellet form and is comprised of a concentrated mixture of pigments, dyes and/or additives to color plastic products. Masterbatch is used in place of fully colored compounded materials largely referred to as pre-color. This option can be more expensive due to volume minimums, inventory requirements and the threat of obsolescence whereas masterbatch mitigates these challenges.

Chroma Color® Liad Feeder

Photo Caption: The ability to dose the masterbatch with absolute precision is a perfect complement for injection molding and extrusion customers looking to reduce their operating costs. For more information about LIAD, contact US Distributor of Chroma Color® Corporation

Even after being convinced that masterbatch is a better colorant option, many processors still debate whether liquid or pellet form is the better option? Both have advantages and disadvantages.

The advantages of liquid color include: effectiveness at extremely low levels, good on long production runs, newer computer-controlled pumps for consistent delivery, and upfront costs can be lower.

The challenges of using liquid color masterbatch are: liquid can cause screw slippage when higher levels are required, liquid carrier resin can separate from the color itself over time requiring offline mixing or peripheral online equipment like agitators, housekeeping issues present a challenge due to the constant threat of equipment malfunctions of hoses and tube sets due to wear and tear.

The advantages of pellet color masterbatch for plastic parts include: reduced housekeeping, zero waste and quick change-overs. Lastly, it avoids all hidden costs like additional hoses and tubes sets, agitation and consolidation that liquid color requires.

The one historical advantage liquid has enjoyed over pellet masterbatch has been rooted in economics. That stated, there is new pellet technology that has come on the scene in the last few years that can both reduce cost and eliminate processing headaches.

Chroma Color®-G2 and G3 Image

Patented G2 and G3 colorants. These pelletized feature the highest-loaded pigment, dye and/or additive packages in the industry. The colorant is exceptionally well dispersed, and can be effectively distributed in large and small parts at a reduced cost.

Coloring Industrial Synthetic Textiles 101

Once you start exploring the types of industrial textiles made from synthetic plastic resin materials you realize there are many products we use or see daily that fall into this category. Today, even more companies are discovering new capabilities and applications for these materials. Hence, this marketplace continues to grow.

A few reasons for wider acceptance of these materials include flexibility, dry fastness, water absorption and performance in harsh environments. Manufacturers easily gain improved performance with a variety of additives, including colors that ensure the product lasts in a wide variety of environments while also looking attractive.


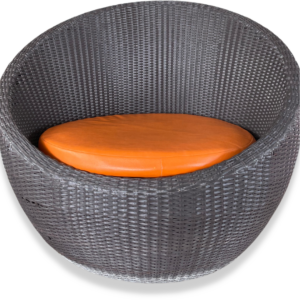
Chroma Color® Textile Outdoor furniture

Typical Textile Plastic Resins Capabilities and Applications:

The plastics resins typically used for industrial textiles include: Polyethylene (PE), Polypropylene (PP), Polyvinyl Chloride (PVC), Thermoplastic Polyurethane (TPU) and more. 

Polyethylene (PE) is the most common plastic used in the world today. Resistant to tears and rips, the material is extremely rugged and durable, making it suitable for industrial applications. Industrial fabrics made from PE are also lightweight, flexible, and resist soiling and staining. In addition, they are non-absorbent, making them less likely to accumulate dirt/ moisture. They are also resistant to bacteria/ mold.

Polyethylene fabrics are typically chosen for applications such as outdoor chairs, tarps, and tents because they are strong and do not stretch. These fabrics can also be used as gardening mulch to block light contributing to the growth of weeds while letting moisture through. Some other common applications include rope, automotive fabrics and the popular re-usable shopping bag.

Polypropylene (PP) has a higher melting point, making it stronger and lighter than polyethylene. The material is also an excellent insulator and can be engineered into a variety of different products or melted down and recycled into something new. Other important properties of polypropylene include toughness, chemical, water, fire resistance and recyclability.

Textile flooring is the most popular use of polypropylene fiber because it has high abrasion resistance and does not absorb dirt or liquids. Other applications include outdoor carpets, golf and tennis courts, the edges of swimming pools and car interiors. This industrial fabric can also be used in construction–to stabilize the ground or to reinforce roads and banks.

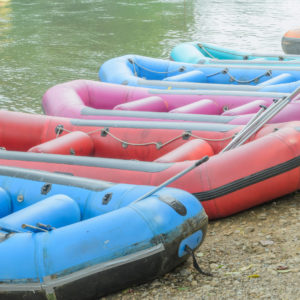
Photo Caption: Marine industrial textiles used for industrial boats

Thermoplastic Polyurethane (TPU) coating:

Thermoplastic polyurethane (TPU) is a very versatile resin. It can be manufactured soft or hard. This material is impact, abrasion, fuel and oil resistant. TPU can be colored and can include additives to protect it from UV rays, funguses and fire.

TPU resin is used to coat textile products such as inflatable boats requiring strength, flexibility, wear resistance, and puncture resistance. It is easy to weld and handle. Other coated textile products include mining screens, conveyor belts, oil booms, barriers/berms, flood spill protection/ control and more.

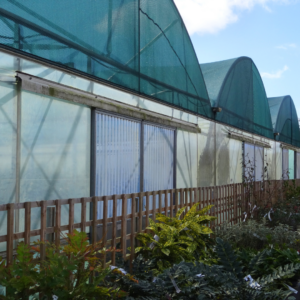
Chroma Color® Greenhouse textile green

Photo Caption: Industrial textiles are used for greenhouse / nursery protection

Polyvinyl Chloride (PVC) contains halogens like chlorine and fluorine that are widely known for being stable. This chemical stability makes the material resistant to stressors like flame, chemicals and oil.

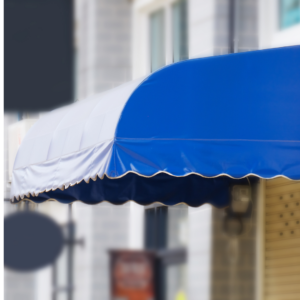
Chroma Color® Business Awning Textile

Photo Caption: Business awnings are a popular application for synthetic textiles.

PVC is used for textile applications such as protective suits for firefighters/ military, industrial tarps, conveyor belts, automotive/ RV headliners, marine sails/ lifejackets, awnings, windscreens, athletic mats and much more.

Common Additives for Plastic Textile Fabrics:

Plastic products are often constantly exposed to UV light that degrades the plastic product quickly. But this can be easily prevented with the addition of a UV additive. Other additive options include flame retardants, anti-static, processing stabilizers, antimicrobial agents, and more. If you think you need additional additives work with your supplier to help you decide what you need and how they will perform for each resin base.

Color Concentrates for Plastic Textiles:

One of the biggest challenges in color use for plastic textiles is matching them to the resin that is used. Initiate a conversation with your color supplier about the resins’ viscosity and melt processing temperatures. This will make the decision on carrier resin, pigments, stabilizers and other additives necessary for the application much easier.

Then, depending upon the material and application, the carrier resin used in the concentrate will be about 30-50%. It is also important to review the molecular weight of that carrier or melt flow rate (MFR). The color concentrate should have higher MFR than the base resin that is being colored in order to produce a good colored part.

After the resin has been clearly established, your conversation can move to color selection. Typically, your supplier will have sample chips or Pantone color charts to pinpoint the desired color for each plastic product or part.

During this selection, bear in mind that colors can look different on the material depending on its gloss, filler and look. For example, lighter colors such as red, orange, and yellow could change color faster compared to darker colors like blue or green.

Looking for unique or custom colors to separate you from your competitors or one that needs to stand out for safety applications such as life jackets or inflatable boats? You can count on color supplier’s like Chroma Color® Corporation to help you choose the best options for your application.

About Chroma Color® Corporation:

CHROMA COLOR Corporation’s textile team has experience helping customers looking for color industrial textiles made from PVC, PP, TPU and PE materials.

Our capabilities include:

  • Fully equipped laboratories to formulate thermoplastics colors and compounds. Colorists thoroughly trained in the theory and practice of spectrophotometry, color measurement, and color science
  • Color formulation, color control, color tolerances, standards, and color faults and their evaluation
  • All facilities meet ISO 9001:2015 standards
  • Adherence to the following regulatory guidelines: FDA Food Contact Compliance, HMF Heavy Metal, Free Formulation, EU & other Global Standards
  • Availability to provide color concentrates in dice, strand, underwater cut, and/or pulverized pellet geometry

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier of the highest quality and the shortest lead times in the plastics marketplace. The business exceeds $160 million in sales due to solid organic growth and targeted acquisitions. Chroma’s extensive technical and manufacturing expertise coupled with its game-changing colorant technologies have surprised and delighted customers for over 50 years in markets such as: packaging, wire and cable, building & construction, consumer, medical, healthcare, lawn & garden, durables, sanitation, recreation and leisure, transportation and more.

Download this material as a PDF

Chroma Color®’s NIR Sortable Black Technology Passes APR Test Protocol for NIR Sorting

ChromaNIR

Chroma NIR Bottles

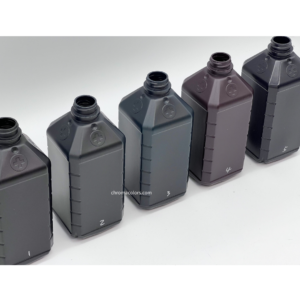
Chroma Color® has developed a specialized formulation path to solving the need for colorant alternatives to Carbon Black as a means to address the recycling of black or dark colors in packaging for improved environmental sustainability.

Chroma Color®’s alternative recipes allow the MRF sorting operations to identify and successfully sort the plastic articles according to the APR NIR Sorting Potential of a Whole Plastic Article. The leading third-party independent lab P.T.I. of Holland, Ohio, conducted all testing and analysis.

ChromaNIR’s Sortable Black Technology is based upon IR reflecting/transparent components using a proprietary combination of specialty dyes and organic pigments. The Chroma Color® path to success allows for expanded exploration of additional Black options, including near-Black and other Dark Color families.

ChromaNIR’s TESTING BASICS:

-The following packages were evaluated using the APR test method: Near Infrared (NIR) Sorting Potential of a Whole Plastic Article (Sort-B-01).

– A total of five recipes were tested using bottles made by extrusion blow molding.

– Three carbon black free formulations were tested in HDPE and One in PP.

– One control formula with carbon black was included.

ChromaNIR’s RESULTS:

– Four Carbon Black Free recipes passed with 100% sortation.

– As anticipated, the one control formula with carbon black failed with 0% sortation.

– A leading independent lab PTI of Holland, OH, tested the plastic articles.

ABOUT ChromaNIR’s OPTIONS:

ChromaNIR’s Sortable Black products, referred to as are available in a variety of resins that include the most commonly used packaging resins, polypropylene, polyethylene, polystyrene, ABS, and PET.

Key features of this color system:

– Inert, heat stable, non-migratory

– Can be used in a variety of polymers

– FDA Compliant

For more information on the testing results, contact us: https://chromacolors.com/contact-us/

CHROMA COLOR:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. With the recent acquisition of Epolin, Chroma Color® is now the recognized leader in the near-infrared (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors.

Chroma Color®’s growth strategy includes robust organic and inorganic growth through nine acquisitions over three years. Chroma Color®’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant, has delighted customers for more than 50 years.

Chroma Color® Corporation Announces the Acquisition of J. Meyer & Sons, Inc.

October 29, 2021, McHenry, IL: Chroma Color® Corporation has acquired J. Meyer & Sons, Inc. a manufacturer of color concentrates and masterbatches for the medical and pharmaceutical markets.

Founded in 1883, J. Meyer & Sons initially was a toy importer from the Black Forest region of Germany. During World War II, the company expanded into the chemical industry, producing driers for the paint and ink industries. During the 1960s, the company moved into plastics to meet the growing demand for customized colors. Today, J. Meyer produces custom and proprietary color masterbatch and compounds.

Chroma Color® is committed to growing our healthcare business through both organic and inorganic activities. The acquisition ofJ. Meyer & Sons further bolsters Chroma Color®’s strengths in supporting our healthcare customers that serve applications like medical devices, medical disposables, and pharmaceutical packaging. The entire team is fully prepared and ready to support J. Meyer & Sons customers during this time of transition and confident their customers will realize immense benefits from Chroma Color®’s wide range of capabilities.

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. Chroma Color®’s growth strategy includes robust organic and inorganic growth through eight acquisitions over three years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant, has delighted customers for more than 50 years.


Chroma Color® Corporation Announces the Acquisition of Color Resource, LLC

 Chroma Color® Color Resources

June 28, 2021-McHenry, IL: Chroma Color® Corporation has acquired Color Resource LLC, a manufacturer of color concentrates for the telecommunications, fiber, building, electronics, and specialty wire markets. Color Resource’s manufacturing plant is located in Leominster, Massachusetts. This acquisition significantly expands Chroma Color® Corporation’s current product offerings in the wire and cable marketplace and other key market segments.

Founded in 2009, Color Resource has provided customers stock and custom color concentrates that meet Munsell, NEMA, RAL, and SAE J-1178 specifications for PVC, PE, PP, and EVA resins. These color concentrates often include additives for UV protection, anti-microbial, flame retardancy, anti-static, or chemical resistance for use in harsh environments.

Chroma Color® President, Howard DeMonte, stated, “We are pleased to now offer our current wire and cable customers with new moisture cure options for emerging markets such as low voltage, automotive, and appliance.  Additionally, Color Resource’s plant in Leominster, Massachusetts, is very close to the Chroma Color®’s facility. This makes the blending of our companies easier on our team members and seamless for our customers.”

This key acquisition of Color Resource brings other technologies and know-how to Chroma Color®, especially for our customers in the wire and cable market. Our entire team is fully prepared and ready to support Color Resource’s customers during this time of transition. We are confident that customers will realize immense benefit as a result of Chroma Color®’s expanded capabilities to support their needs.

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. Chroma Color®’s growth strategy includes robust organic and inorganic growth through six acquisitions over three years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant has delighted customers for more than 50 years. For additional information, please visit www.chromacolors.com.

Color Resource, LLC:

Color Resource manufactures premium quality color concentrates for the wire and cable, profile extrusion, and injection molding industries. All products are RoHS and REACH compliant. Color Resource offers an in-stock full-range line of Munsell and NEMA colors in PVC, PE, and standard EVA color concentrates exhibiting excellent electrical properties. Color Resource’s moisture cure XLPE compounds meet the needs of the low-voltage, automotive, and appliance wire markets.

https://color-resource.com/

From Prison to Plastics Manufacturing Podcast and Article

Chroma Color® Corp. has an unusual way of finding workers: It recruits mostly from the local prison.

Finding and keeping a solid workforce is a vexing problem for all manufacturers, but the company leans on hiring convicted felons.

While employing prisoners might scare off some, Vice Chairman Matt Barr said the company started hiring from the penitentiary in 1990 because it was having trouble finding and retaining factory workers. Altruism, seeing people from prison get a new start, has certainly become part of the company’s motivation. But the effort has clear value to the bottom line, he said.

“It’s been a great tool for us to develop a consistent workforce, train them according to our needs and ultimately as important or more important, give these gentlemen an opportunity to get some footing so that when they come out of the prison system they have an opportunity to turn their lives around,” Barr said.

Listen to the podcast on Plastics News site:

https://www.plasticsnews.com/article/20171206/MULTIMEDIA03/171209947/former-inmates-start-a-new-life-at-carolina-color

Or check out the articles:

https://www.plasticsnews.com/article/20170515/NEWS/170519947/from-prison-to-a-plastics-factory

https://www.plasticsnews.com/article/20170515/NEWS/170519946/society-doesn-t-see-the-success-stories

Chroma Color® Corporation Introduces NIR Sortable Black Color Concentrate Solution

Chroma Color® NIR Black

Material Recycling Facilities (MRFs) use IR (infrared) and NIR (near infrared) sorting technology to increase yield, improve throughput rates, and increase profitability.  The challenge with this technology is its inability to properly identify and accurately sort black colored plastic products.  Carbon black absorbs the light emitted from the IR devices and prevents the successful identification of the type of plastic. These unsorted black plastic products are rejected and, in most cases, end up in landfills.

Brand owners have published aggressive sustainability goals requiring a quantum leap in the recyclability of plastic articles. It is not acceptable to loose plastic articles to landfill solely because they are black or very dark in color.   Significant resources have been devoted to creating black branded products, and viable practical solutions are required.  Rather than sacrificing the brand’s aesthetic desires, the best option is to maintain brand recognition and replace carbon black with an alternative black coloring technology.

Chroma Color® now offers a solution to this problem.  A carbon black alternative that does not sacrifice brand aesthetics but allows the MRF sorter to accurately and repeatedly identify and sort the plastic article.

Chroma Color®’s NIR sortable black technology is based upon IR reflecting/transparent pigments and proprietary combination of dyes and organic pigments.

This product is referred to as “NIR Sortable Black ” and is available in a variety of resins that include the most common packaging resins; polypropylene, polyethylene, polystyrene, ABS and PET.

Key features of this color system:

Inert, heat stable, non-migratory

Can be used in a variety of polymers

FDA Approved

About Chroma Color®

Chroma Color® Corporation is a technology-leading specialty color and additive masterbatch supplier delivering critical aesthetics, technical innovations, and sustainable solutions to plastics processors and brand owners. Chroma Color®’s growth strategy includes robust organic and inorganic growth, having made six acquisitions over the last three years. Chroma Color®’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant and light management technologies, have delighted customers for over 50 years.