Plastic Packing Trends and How to Choose the Best Color Concentrates to Meet These Trends

Trends in Packaging in 2026 and Beyond

A major trend in packaging is the shift toward smarter, advanced solutions. These include digital watermarks for better sorting and recycling, as well as sensors that track freshness and supply‑chain conditions. Brands are also reducing material use through lightweight designs and adapting packaging for e‑commerce and convenience. Overall, plastic packaging is evolving to balance cost, functionality, and sustainability amid expanding consumer and regulatory pressures.

The rapid adoption of GLP‑1 drugs is significantly affecting demand for plastic packaging. These medications rely on plastic‑heavy delivery systems—such as single‑use autoinjector pens, protective caps, and sterile packs—driving large‑scale production and investment in medical‑grade plastics. They also require cold‑chain packaging due to refrigeration needs.

Chroma Color for Medical products and devices

Because GLP‑1 drugs reduce appetite, consumers are buying less food, especially packaged snacks, lowering demand for some plastic food packaging. This decrease is partly offset by growing interest in smaller portions and resealable formats. At the same time, the rise in single‑use medical plastics, including injector pens and sharps containers, is increasing waste concerns and highlighting the need for more eco-friendly materials and recycling solutions in healthcare.

How to Choose the Right Color Concentrate to Meet Your Current Plastic Packaging Needs

It is essential in today’s business environment to choose the best color concentrate technology that delivers highly consistent, high-performance color to your packaging, improving both processing effectiveness and final product quality. Look for advanced formulations that allow for lower let-down ratios, meaning manufacturers can achieve the same color intensity with less material—cutting overall costs and improving sustainability. The technology ought to enhance dispersion, resulting in smoother color uniformity, fewer production defects, and more predictable performance across multiple resin types and applications.

Chroma Color Concentrates Pellets

You should also ask yourself: Is this color concentrate engineered for faster processing and reduced cycle times to ensure throughput without impairing color precision or durability? Does the concentrate’s thermal stability support demanding packaging processes, including thin-wall designs and high-speed extrusion or injection molding? Together, these advantages will help you boost packaging performance, reduce waste, and improve operations.

The Benefits of Switching from Liquid Color to Color Concentrates:

Switching from liquid color to high-performance color concentrate technology offers several important advantages that can significantly improve manufacturing performance and reduce total production costs. High-performance systems provide far more precise colorant delivery, resulting in consistent, repeatable color with minimal variation from batch to batch. Because these technologies meter color directly into the process, they eliminate the mess, storage challenges, and contamination hazards often associated with liquid color. They also reduce cleanup time and simplify changeovers, permitting operators to move between colors more quickly with less downtime. In many cases, you can achieve the same—or better—color strength while using less additive. The combination of accuracy, cleanliness, reduced waste, and lower operating costs makes these systems a strong upgrade over traditional liquid color.

How Color Concentrate Drug Master Files (DMFs) for Medical Plastic Packaging Makes Your Life Easier

Drug Master Files offer medical packaging companies a substantial regulatory and operational advantage by providing pre-vetted, FDA-reviewed documentation for colorants used in pharmaceutical and healthcare products. This reduces the burden of material qualification, speeds time to market, and simplifies compliance for devices such as syringes, caps, connectors, and diagnostic components. With DMFs in place, you can be confident that your color concentrate is safe, consistent, and traceable—critical factors for your medical-grade packaging that must meet strict performance and regulatory requirements.

A Good Color Concentrate Option for Your Plastic Packaging

Chroma Color G3 Logo

Chroma Color’s G3 technology delivers strong value by providing high-efficiency color concentrates that improve processing performance while cutting overall material costs. G3’s advanced dispersion enables rich, uniform color at significantly lower let-down ratios, helping manufacturers use less concentrate without sacrificing quality. Chroma’s patented G3 technology can also provide highly loaded concentrates containing laser-marking additives. The formulation also allows faster cycle times, excellent thermal stability, and cleaner processing, which together reduce waste, improve production efficiency, and improve sustainability across a wide range of plastic packaging applications.

To learn more about G3 and Chroma Color Corporation, visit: chromacolors.com.

Chroma Color Here to Help Meet the Growing Demands of Cables for Data Centers

Chroma Color Data Cable Options

As global data consumption continues to surge, the demand for high-performance data cables has grown exponentially. From hyperscale data centers to industrial automation systems, reliable connectivity is critical—and cables play a vital role in overall performance of the facility.

Chroma Color Capabilities: Tailored for Every Application

Chroma Color’s advanced color technology supports a wide spectrum of material options across multiple insulation and jacketing materials, ensuring that every cable type meets the needs of the variety of cable used for the data center. This flexibility empowers wire and cable manufacturers to meet stringent requirements without compromising durability or performance.

  • FEP (Fluorinated Ethylene Propylene): Known for its exceptional chemical resistance, high-temperature stability and excellent dielectrics, Chroma Color delivers vibrant, consistent colors on FEP for demanding environments.
  • ETFE (Ethylene Tetrafluoroethylene): Ideal for aerospace and harsh industrial settings, Chroma Color ensures, excellent dielectrics, sharp fade-resistant colors that maintain clarity under extreme conditions.
  • ChromaXLPEUltra (Cross-Linked Polyethylene): For high-voltage and data applications, Chroma Color provides robust color solutions that withstand thermal and mechanical stress.
  • PVC (Polyvinyl Chloride): A versatile and cost-effective option, Chroma Color offers a full palette of standard colors in addition to custom color matching expertise for PVC jackets, supporting easy identification in commercial and residential installations.
  • EVA (Ethylene Vinyl Acetate): With its flexibility and resilience, EVA benefits from Chroma Color’s precision coloring for specialty cable designs.

Important Considerations to Keep in Mind for Colorants & Additives

  • Pigments must tolerate:
    • High extrusion temperatures
    • Long heat aging cycles
  • Poor pigment selection and dispersion can lead to:
    • Discoloration
    • Reduced UV or heat resistance
    • Spark failures
  • Some colorants can negatively affect flame or thermal performance if not formulated correctly.

You can rely on Chroma Color to Help you meet these material challenge: We will help you maintaining color consistency without compromising heat or fire ratings.

Material Heat-Related Challenges (Critical)

  1. Insulation & Jacket Thermal Resistance
  • Heat during extrusion can degrade polymers (PVC, PE, XLPE, LSZH).
  • Overheating causes:
    • Brittleness or cracking
    • Poor dielectric performance
    • Reduced flame resistance
  • Tight process windows are required to avoid polymer scorching or inconsistent wall thickness.
  1. Compliance & Safety Standards
  • Heat performance must meet:
    • UL, IEC, ISO standards
    • Flame retardancy (CMP, CMR, CMX ratings)
  • Fire testing (plenum, riser) exposes weaknesses in thermal stability.
  • Failures often stem from improper heat aging resistance.

Key Material Takeaway

In data cable manufacturing, materials define thermal limits. The right combination of conductor quality, insulation polymer, jacket compound, color / additive package determines whether a cable can handle modern demands like high-speed data, PoE (Power over the Ethernet) power loads, CAT5/6/6e, Robotics and strict fire codes without overheating or failing prematurely.

Chroma Color is committed to material compatibility and color to ensure that every of your data cables meets both functional and aesthetic requirements. To learn more contact us

Download the data cable flyer

Click here learn about our ChromaXLPEUltra product

ChromaGlowUltra Masterbatch Colors Meet Growing Demands from Plastic Molders

Chroma Photoluminescent Color


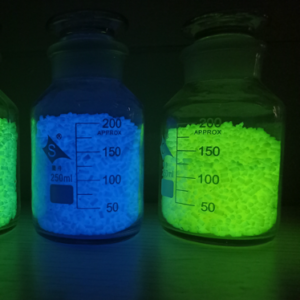
ChromaGlowUltra is also known as a glow-in-the-dark color concentrate, have gained popularity in recent years due to their unique properties and ability to create eye-catching visual effects. For example, photoluminescent color concentrates are increasingly being used in safety applications such as emergency exit signs, egress path markings, and safety equipment. This is because photoluminescent materials are reliable and can be charged by both natural and artificial light, ensuring that they remain visible even in low-light or dark conditions.

Chroma Color® continues to explore new materials and technologies to improve the properties of photoluminescent color concentrates for our customer to be more efficient and brighter than traditional pigments.

The Benefits of ChromaGlowUltra Masterbatch Includes:

– Rapid activation yielding hours of glow

– Light stable formulation (fade resistant)

– Custom-tailored for glow longevity and brilliance

– Designed for specific life safety applications

– Enhance and differentiates outdoor or indoor applications

To ensure customers of ChromaGlowUltra masterbatch will yield hours of glow. We had products molded using Chroma Color®’s Glow tested by an outside laboratory resulting in measurements of 32 hours of glow time. To examine the variety of resins tested and results download the pdf

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others.

With the recent acquisition of Epolin, Chroma Color® is now the recognized leader in the near-infrared (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors.

Chroma Color®’s growth strategy includes robust organic and inorganic growth through nine acquisitions over three years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its game-changing colorant, has delighted customers for over 50 years.

Chroma Color® Corporation Herres Named to Manufacturers Association Board of Directors

Chroma Color®'s Joe Herres Board Member of NAM

Washington, D.C. – The National Association of Manufacturers announced that Joe Herres CEO of Chroma Color® Corporation, has been named to the NAM Board of Directors. Herres will join the NAM Board to bolster the association’s leadership in policy advocacy, legal action, workforce solutions and operational excellence. He will help the industry advance a manufacturing competitiveness agenda that promotes opportunity and prosperity for all Americans.

Founded in 1895, the NAM, guided by its Board of Directors, is the largest industrial trade association in the United States. The NAM is the nation’s most influential manufacturing advocate, and its membership includes some of the world’s most iconic brands and many of the small manufacturers that power the U.S. economy. Approximately 85% of the NAM’s members are small and medium-sized businesses. Executives on the NAM Board, which comprises leaders representing companies of all sizes in every industrial sector, are the driving force behind the NAM’s efforts.

The NAM is a one-stop shop for manufacturers, telling the story of our industry and equipping manufacturers with invaluable resources through news and insights, thought leadership and partnerships with our digital transformation division, the Manufacturing Leadership Council; our 501(c)3 workforce development and education affiliate, the Manufacturing Institute; and our innovation management division, the Innovation Research Interchange.

The NAM and its members are at the forefront of every important policy debate, focusing on solutions to help the industry compete in the global economy and to help the country address manufacturing policy priorities ranging from renewing pro-growth tax policies and restoring regulatory certainty to securing energy and building a workforce of the future.

“Joining the NAM Board is a privilege and an opportunity to advance the vital work of strengthening manufacturing in the U.S.,” said Herres. “I am committed to collaborating with industry leaders to advocate for policies that will promote competitiveness and job creation. The manufacturing sector is essential to America’s economic resilience, and I look forward to ensuring our industry continues to thrive for the benefit of all Americans.”

“Joe is a proven leader who is committed deeply to the success of our industry, and the NAM will be stronger thanks to his service on our Board of Directors,” said NAM President and CEO Jay Timmons. “We are in a defining moment for manufacturing in the U.S. as we advocate for a clear, actionable and commonsense strategy from the federal government that will increase investment in the U.S. and make us more successful. Joe will be a partner in advancing a competitiveness agenda that will amplify the voices and efforts of manufacturers across America. I look forward to working together as advocates for manufacturing in the U.S. while we advance the values that have made America exceptional and our industry strong—free enterprise, competitiveness, individual liberty and equal opportunity.”

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, among others. Chroma Color®’s growth strategy includes a deep focus on organic growth as well as inorganic growth through several strategic acquisitions over recent years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its market-leading colorant, has delivered high value to customers for more than 50 years. chromacolors.com.

-NAM-

The National Association of Manufacturers is the largest manufacturing association in the United States, representing small and large manufacturers in every industrial sector and in all 50 states. Manufacturing employs nearly 13 million men and women, contributes $2.93 trillion to the U.S. economy annually and accounts for 53% of private-sector research and development. The NAM is the powerful voice of the manufacturing community and the leading advocate for a policy agenda that helps manufacturers compete in the global economy and create jobs across the United States. For more information about the NAM or to follow us on Twitter and Facebook, please visit www.nam.org.

733 10th St. NW, Suite 700 • Washington, DC 20001 • (202) 637-3000

What is the Smarter Choice for Plastic Manufacturing…Color Concentrates or Liquid Color?

Over the past decade, consumer packaged goods (CPG) companies have increasingly prioritized cost reduction. While efforts have largely focused on innovations in package design and construction, attention has also shifted to other cost factors, such as colorants and design features.

Traditionally, CPG companies relied on the expertise of their molding partners in these areas. However, in recent years, colorant suppliers have taken a more proactive approach, presenting their cost-saving solutions directly to corporate decision-makers.

This shift has led to the growing adoption of liquid color in the packaging industry, because in some cases it has demonstrated ability to lower let-down ratios and reduce overall costs compared to traditional color concentrates. Despite these benefits, many processors remain hesitant due to the housekeeping challenges and high scrap rates often associated with liquid color.

 Overview of Liquid Color
Chroma Color® Liquid Color Alternative

Advancements in liquid colorant dosing systems over the past decade have greatly enhanced their user-friendliness, providing cleaner and easier handling solutions tailored to industry requirements. Liquid colorants have long delivered vibrant hues at low use rates, offering excellent color distribution ideal for tints and transparent applications. For instance, liquid colorants can achieve some pearlescent and metallic effects, enhancing shelf appeal for brand owners and packaging designers.

Additionally, liquid colorants can be processed at lower temperatures than traditional masterbatch, avoiding heat history degradation and eliminating pre-decomposition concerns. This makes them a reliable and efficient choice for achieving striking visual effects without compromising material integrity.

On paper, liquid color may seem cost-effective, promising aesthetic benefits at reduced expenses. However, the hidden drawbacks often complicate the overall production process.

Challenges of Liquid Color:

  • Complex Equipment Needs: Liquid color requires specialized pumps and hoses to integrate properly, complicating operations. For example: If a line stops and the equipment isn’t tied into the screw signal correctly the liquid pump will keep dosing, flooding the barrel with color.

In addition, Liquid is delivered through polyethylene tubes which can wear out and rupture, causing spills.  Additionally, these tubes are consumables not provided by the manufacturer and need to be purchased by the molder.

  • Handling Inefficiencies: High risks of spills and constant equipment maintenance make liquid color messy and inefficient. For example, liquid color often causes screw slippage, especially at higher letdown ratios, which results in the constant monitoring of the machine and severe delays in production.  When a liquid container empties, it often does so with no warning. This requires the machine to be stopped until the new container is ready to run and again, causes delays in production.

Liquid color also has a tendency when used for long periods of time to cause staining of the screw of the manufacturing machine The limited shelf life and frequent separation issues lead to waste.

  • Resin Compromises: Liquid color displaces resin, requiring more material to maintain shot weight, which can increase costs unexpectedly. For instance, a lower letdown ratio (LDR) may look appealing but adds resin expenses, diminishing perceived savings. In addition, liquid needs to be stored in temperature-controlled areas.  Additionally, shipping liquid in cold weather can allow it to freeze, ruining the color.
  • Waste & Sustainability: Liquid color cannot be fully used from containers, leading to scrap rates of up to 10%. Combined with disposal issues requiring hazardous waste removal, this contributes significantly to environmental concerns. Plus, when using regrind, the fines can mix with liquid and create clumps that block the flow of pellets through the feed throat.

The Efficiency of New Technology of Color Concentrates

Newer color concentrate technology offers a superior alternative that minimizes these inefficiencies. Unlike liquid color, advanced pelletized concentrates eliminate the mess, waste, and complex equipment while offering consistent color results across various applications.
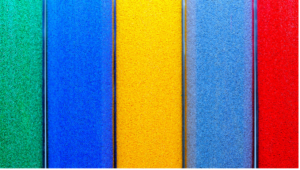
Chroma Color® Pellet Color Concentrates

Advantages of Color Concentrate Pellets:

  • Sustainability: Liquid color’s carbon footprint is significant, with oil-based carrier systems adding to environmental impact. This technology’s carrier system uses fewer raw materials and reducing carbon output.
  • Ease of Use: These pellets integrate seamlessly into production lines, compatible with standard feeding systems. No pumps, no spills—just easy, efficient coloring.
  • Maximized Usage: Unlike liquid color, this technology allows for 100% use, reducing waste and ensuring every pellet contributes to the product.
  • Reduced Scrap and Downtime: Liquid color systems often cause scrap and require frequent purging, but these color concentrates pellets enable faster color changeovers with minimal waste, optimizing production efficiency.
  • Simplified Disposal: These pellets are also non-hazardous and disposed of in traditional waste streams, unlike liquid color, which needs special disposal and adds to a higher carbon footprint.

Comparing the Environmental Impact
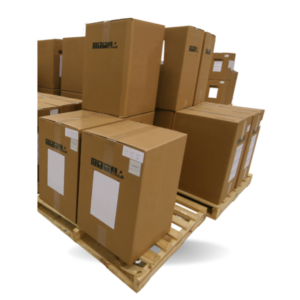
Chroma Color® Pellet Color Concentrates Shipping

Packaging and Shipping:  A 1,000-pound order of this technology is packaged in Sustainable Forestry Initiative (SFI) rated cardboard and weighs about 25 pounds including the lid. Most processors have liquid color delivered in 5-gallon buckets so they can agitate the color before use. Obviously, pellets do not need to be agitated. To ship 1,000 pounds of liquid color in plastic buckets is roughly 100 pounds of packaging material used to ship the liquid color vs 25 lbs. of the new pellet technology.

Some liquid companies have touted a “Pump in a Drum” system for reusable packaging, but keep in mind doing this adds another shipment back to the manufacturer and increases the carbon footprint of the packaging in the life cycle assessment.

“Cradle to Grave” Sustainability: The complete lifecycle of this newer color concentrate is designed to be environmentally friendly, with fewer emissions and more efficient waste management. Liquid color’s extra shipments for hazardous waste disposal and inefficient usage only add to its environmental burden.

Why Chroma Color®’s ChromaGSeries Is the Future
ChromaGSeries

Chroma Color®’s patented G2 and G3 technologies represent a breakthrough in the plastics industry. By combining the dispersion quality of liquid color with the ease and efficiency of pellets, G2 and G3 achieve vibrant, uniform colors at lower letdown ratios. This means manufacturers benefit from cost savings without sacrificing quality.

To explore how G2 and G3 can transform your production, visit: Chroma Color® G-Series.

About Chroma Color® Corporation
Chroma Color® delivers unparalleled color solutions for industries ranging from packaging to healthcare. With a focus on innovation and customer satisfaction, our G-Series technology and strategic growth have established us as industry leaders for over 50 years. Learn more at www.chromacolors.com.
Chroma Color® Expands Footprint with West Coast acquisition of Spectra Color

Chroma Color® and Spectra Color logos

<12/20/2024>, McHenry, IL: Chroma Color® Corporation (“Chroma Color®” or “Chroma”) continues to grow its manufacturing footprint along with its portfolio of colorant and additive technologies with its recent acquisition of Spectra Color, Inc. (“Spectra Color” or “Spectra”) a custom manufacturer of colorants and pre-colored resin compounds. Spectra also manufactures a proprietary resin primarily made from linear low-density polyethylene, predominantly used in the rotational molding industry.

Located in Corona, California, Spectra is a leading provider of masterbatch and color-matching services with custom blending capabilities. Founded in 1976, they have supplied the plastic industry with high quality thermoplastic compounds, colorants, additives, and value-added resins for over 45 years. Spectra serves diverse end-markets, including medical, healthcare, agriculture, consumer products, among others.

Spectra CEO, Bob Shedd, said, “We are thrilled to join forces with Chroma Color®. Chroma’s strong market reputation and shared vision for the business make this partnership a perfect fit. By combining  our technological expertise, we can deliver a powerful competitive advantage, enhance performance, and create even greater value for our customers.”

“Chroma Color® is dedicated to driving growth through both organic initiatives and inorganic growth opportunities. The acquisition of Spectra Color underscores our commitment to expanding our geographic reach and enhancing our product offerings to better serve our customers,” stated Joe Herres, Chroma Color® Corporation, CEO. “The entire team is fully prepared to support Spectra’s customers during this transition, and we are confident they will experience significant value from Chroma’s extensive capabilities and resources.”

Chroma Color®:

Chroma Color® Corporation is a leading specialty color and additive concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, among others. Chroma Color®’s growth strategy includes a deep focus on organic growth as well as inorganic growth through several strategic acquisitions over recent years. Chroma’s extensive technical leadership and manufacturing expertise, coupled with its market-leading colorant, has delivered high value to customers for more than 50 years. chromacolors.com

Chroma Color® Corporation Introduces New Capability to Mold 3D Samples for Enhanced Color Visualization

Chroma Color® Sample Program

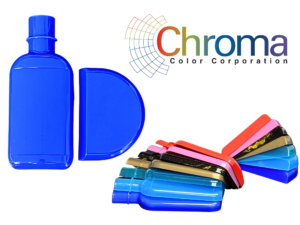
Chroma Color® Corporation, a leading supplier of innovative color concentrates, is proud to announce a new capability that revolutionizes the way customers can experience and evaluate color options. Moving beyond traditional flat color chips, Chroma Color® now offers the ability to mold samples, showcasing their colors in a more dynamic and realistic 3D form.

This advancement allows customers to see how colors appear on an actual sample, providing a comprehensive view of hues, effects, and undertones in real-world applications. By moving from standard step chips to molded samples, Chroma Color® enhances the decision-making process, ensuring clients have a more accurate understanding of how their chosen colors will look on finished products.

“Our new molded color samples offer a significant advantage for our customers,” said James Walsh, VP of Technology, Chroma Color® Corporation. “It’s all about providing a more tangible, three-dimensional experience to better meet the creative and functional needs of our clients.”

For more information on how Chroma Color®’s new sample bottle capability can benefit your project, contact us here: https://chromacolors.com/contact-us/

Download this product pdf: https://chromacolors.com/wp-content/uploads/2024/11/Chroma-Colors-3D-Sample-Program-2024.pdf

About Chroma Color®

Chroma Color® Corporation is committed to delivering exceptional color solutions for a variety of industries, including packaging, consumer goods, and healthcare. With a focus on innovation and quality, Chroma Color® continuously pushes the boundaries of what’s possible in color technology.

Chroma Color®’s growth strategy includes robust organic and inorganic growth through nine acquisitions over three years. Chroma’s extensive technical leadership, manufacturing expertise, and its game-changing G-Series colorant, has delighted customers for over 50 years.

The Power of G2 Color Concentrates for Large Plastic Molded Parts: A Game-Changer for Construction, Utilities, and Material Handling Markets

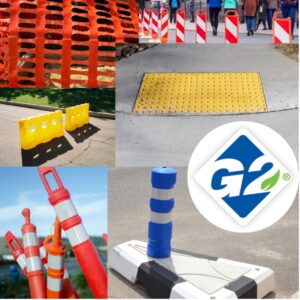
Chroma Color® G2 for large construction products

In the world of construction, utilities, and material handling efficiency, durability, and cost-effectiveness are paramount. Chroma Color® Corporation’s G2 color concentrates have emerged as a game-changer, providing a solution that not only enhances the aesthetic appeal of large -molded parts but also significantly reduces overall costs.

Unmatched Effectiveness

G2 color concentrates are designed to deliver superior performance in large-scale molding applications. Their advanced formulation ensures consistent and vibrant colors, enhancing the visual appeal of products ranging from construction equipment to safety gear and utility components. The high pigment load in G2 concentrates ensures excellent color strength and uniformity, even in the most demanding applications.

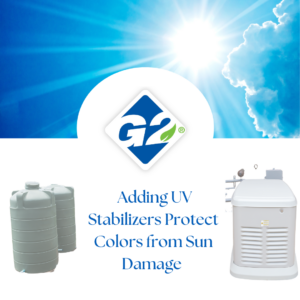
Chroma Color® UV additives

In addition, Chroma Color®’s G2 color concentrates can be enhanced with UV additives, providing superior protection against the harmful effects of UV rays from the sun. This added UV stability ensures that colors remain vibrant and do not degrade quickly, extending the lifespan and aesthetic appeal of large -molded parts used in outdoor environments.

Cost Efficiency

One of the standout features of G2 color concentrates is their ability to lower overall production costs. The concentrates are engineered for high dispersibility, meaning they blend seamlessly into various polymers, reducing the amount of colorant needed. This efficiency translates into cost savings on raw materials.

Additionally, G2 concentrates:

  • Minimizes the need for frequent color adjustments,
  • Reduces downtime
  • Enhances production efficiency.

Versatility Across Markets

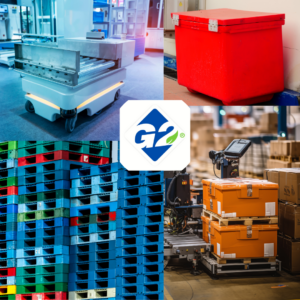
Chroma Color® G2 for Material handling products

Chroma Color®’s G2 concentrates are versatile and adaptable, making them ideal for the diverse needs of the construction, safety, and utilities markets. In construction, they are used to mold durable and visually appealing components like pipes, fittings, and housing materials. The safety industry benefits from the high visibility and durability of G2-colored safety gear, ensuring compliance with safety standards while maintaining cost-effectiveness. In utilities, the concentrates contribute to the production of robust and reliable parts such as electrical enclosures and water management systems.

Environmental Benefits

Beyond cost and performance, G2 color concentrates align with sustainability goals. Chroma Color® is committed to environmentally responsible manufacturing practices, and G2 concentrates are formulated to minimize waste and energy consumption during production. This eco-friendly approach not only benefits the environment but also appeals to companies striving to meet their sustainability targets.

Conclusion

Chroma Color® Corporation’s G2 color concentrates are a testament to innovation in the field of large-scale molding. Their effectiveness, cost efficiency, versatility, and environmental benefits make them an invaluable asset in the construction, safety, and utilities markets. By choosing G2 concentrates, manufacturers can enhance their product offerings, streamline production processes, and contribute to a more sustainable future. Learn more at https://chromacolors.com/products/g-series/

Chroma Color® Exhibiting at Compounding World 2024 Booth # C1526

Chroma Color® Compounding World 2024

Chroma Color® Corporation is a leading specialty color concentrate supplier serving diverse markets, including wire and cable, packaging, healthcare, pharmaceutical, consumer products, and others. With the acquisition of Epolin, Chroma is also the recognized leader in the near-infrared (NIR) absorptive dye industry, producing proprietary blends to suit the eye protection and light management sectors. Stop by booth C1526 to talk to the Chroma Color® about our color concentrates and masterbatches that includes G-Series, UltraPET, ChromaPCRPET, ChromaNIR, Bio-Compostable option, and more.

The Compounding World Expo is being held in Cleveland, OH, on November 13-14, 2024. Cleveland is the plastics hub of North America and this event caters to the entire compounding supply chain where you can network with peers, gain insights from experts, and explore cutting-edge exhibits – all for FREE. To register visit: https://na.compoundingworldexpo.com

Also you can gain a broader perspective with the co-located expos: Plastics Extrusion World Expo, Plastics Recycling World Expo, and Polymer Testing World Expo that offer cross-industry insights. Our dynamic conference program features technical presentations, industry debates, and insightful seminars across four dedicated theaters.